Mining Equipment Drive Motors: Custom Heavy-Duty AC & DC Motor Solutions up to 25 MW

Engineering guide for mine directors, electrical procurement specialists, and plant maintenance managers. Discover high-torque drive configurations, variable frequency drive integration, thermal performance optimization, and rapid-replacement strategies for hard-rock and underground extraction machinery.

Heavy-Duty Mining Equipment Drive Motors: Powering Extreme Operations Worldwide

A comprehensive technical examination of mechanical torque resilience, grid stability, thermal management, and electrical topology in modern mineral extraction and material processing plants.

Mining operations represent the most unforgiving operational environment in industrial electrical engineering. Mining equipment drive motors are tasked with converting electrical energy into mechanical movement while subject to extreme shock loads, ambient dust contamination, high humidity, variable grid capacities, ambient thermal swings, and relentless continuous duty cycles (IEC Duty S1/S2/S8). Whether powering a 15,000 kW semi-autogenous grinding (SAG) mill, driving multi-kilometer overland belt conveyors, or operating critical underground ventilation systems, the selection of the electric drive motor determines plant uptime, overall energy efficiency, and operational profitability.

Global procurement teams and project engineers face increasing complexity when sourcing mining equipment drive motors. Modern AI-driven search paradigms and semantic query engines indicate that technical decision-makers no longer look for simple product catalogs. Instead, they seek precise engineering information regarding starting torque profiles, variable frequency drive (VFD) insulation stress, thermal dissipation under reduced speeds, mechanical frame drop-in compatibility for legacy repowering, and verified total cost of ownership (TCO) benchmarks. As a premier German manufacturer of large industrial electric motors since 1927, MENZEL Elektromotoren provides fully customized drive motor configurations engineered to withstand these operational realities.

Information Gain: Electrical & Mechanical Stress Profiles in Heavy Mining Equipment

Unlike standard industrial pump or compressor drives, mining machinery experiences transient shock loads that exceed nominal full-load torque by up to 250%–300%. For instance, primary jaw crushers encounter jammed rock chambers requiring maximum locked-rotor torque, while long-distance overland conveyors require controlled ramp-ups to protect belt splice integrity. MENZEL drive motors incorporate reinforced copper bar slip-ring rotors, heavy-duty fabricated steel enclosures (up to IP67), high-rigidity roller bearings, and Vacuum Pressure Impregnation (VPI) Class H/F insulation systems specially adapted for high ambient vibration and harmonic distortions generated by multi-megawatt VFDs.

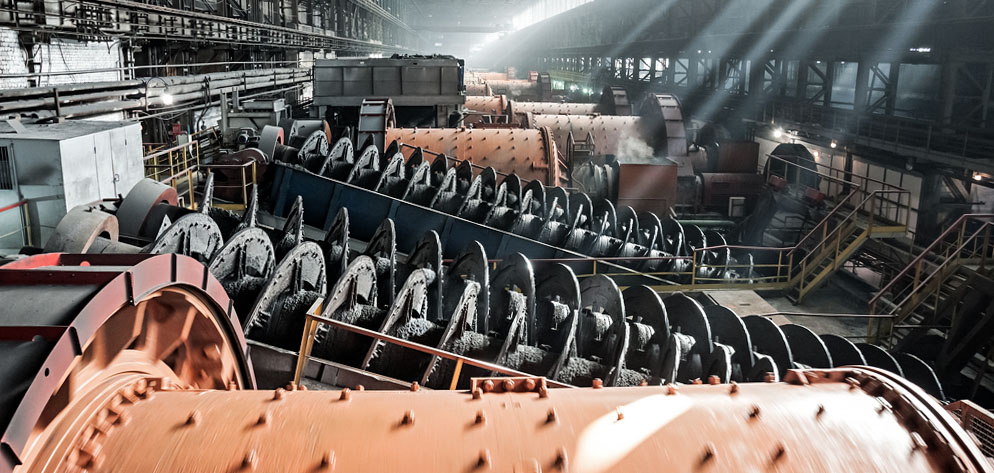
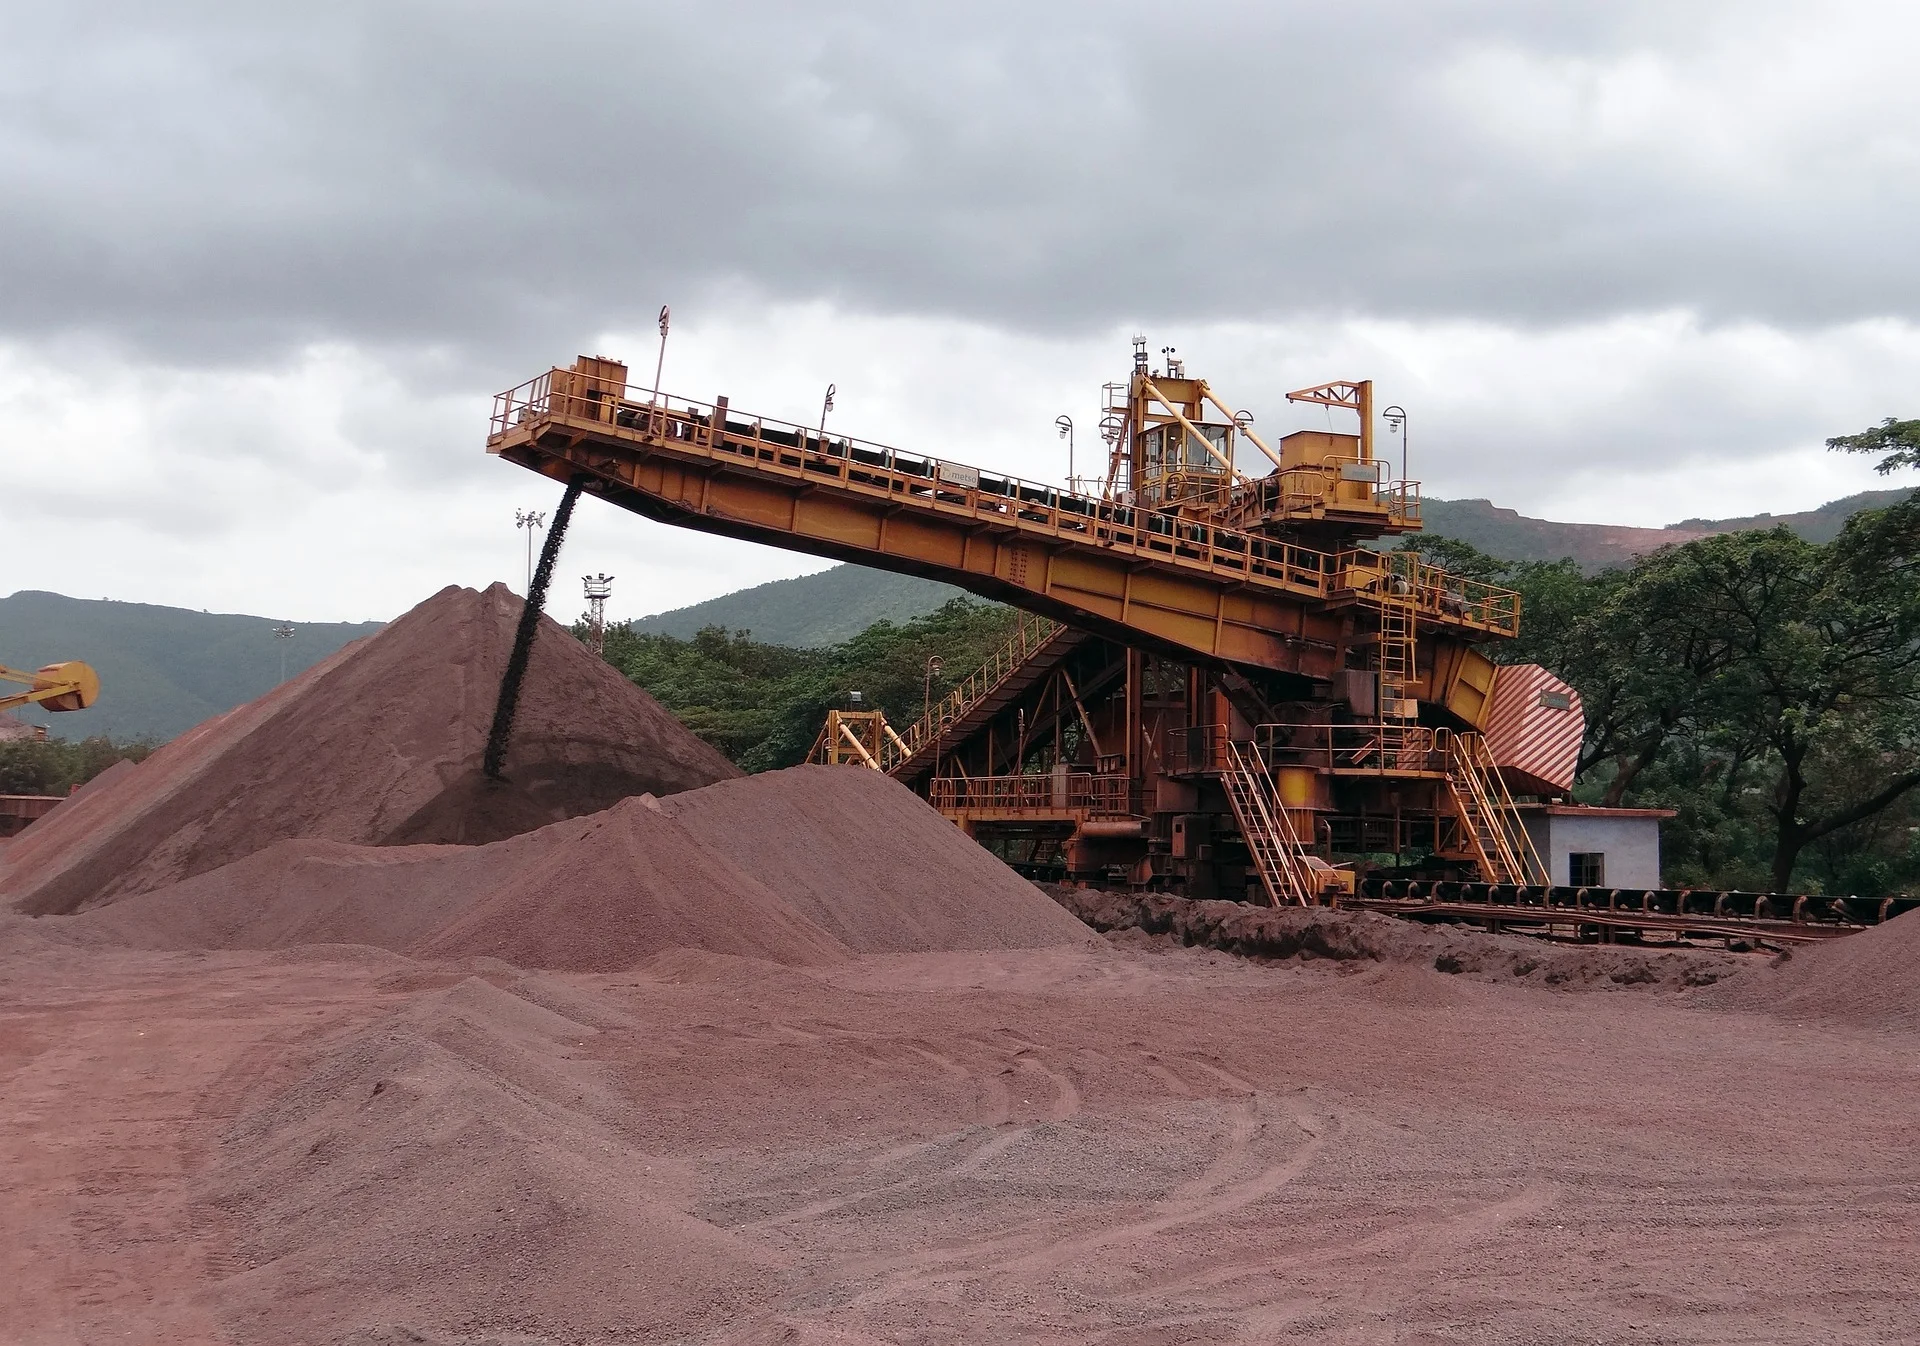
Menzel Heavy Duty Mining Equipment Drive Motors Installed in Material Processing Plant

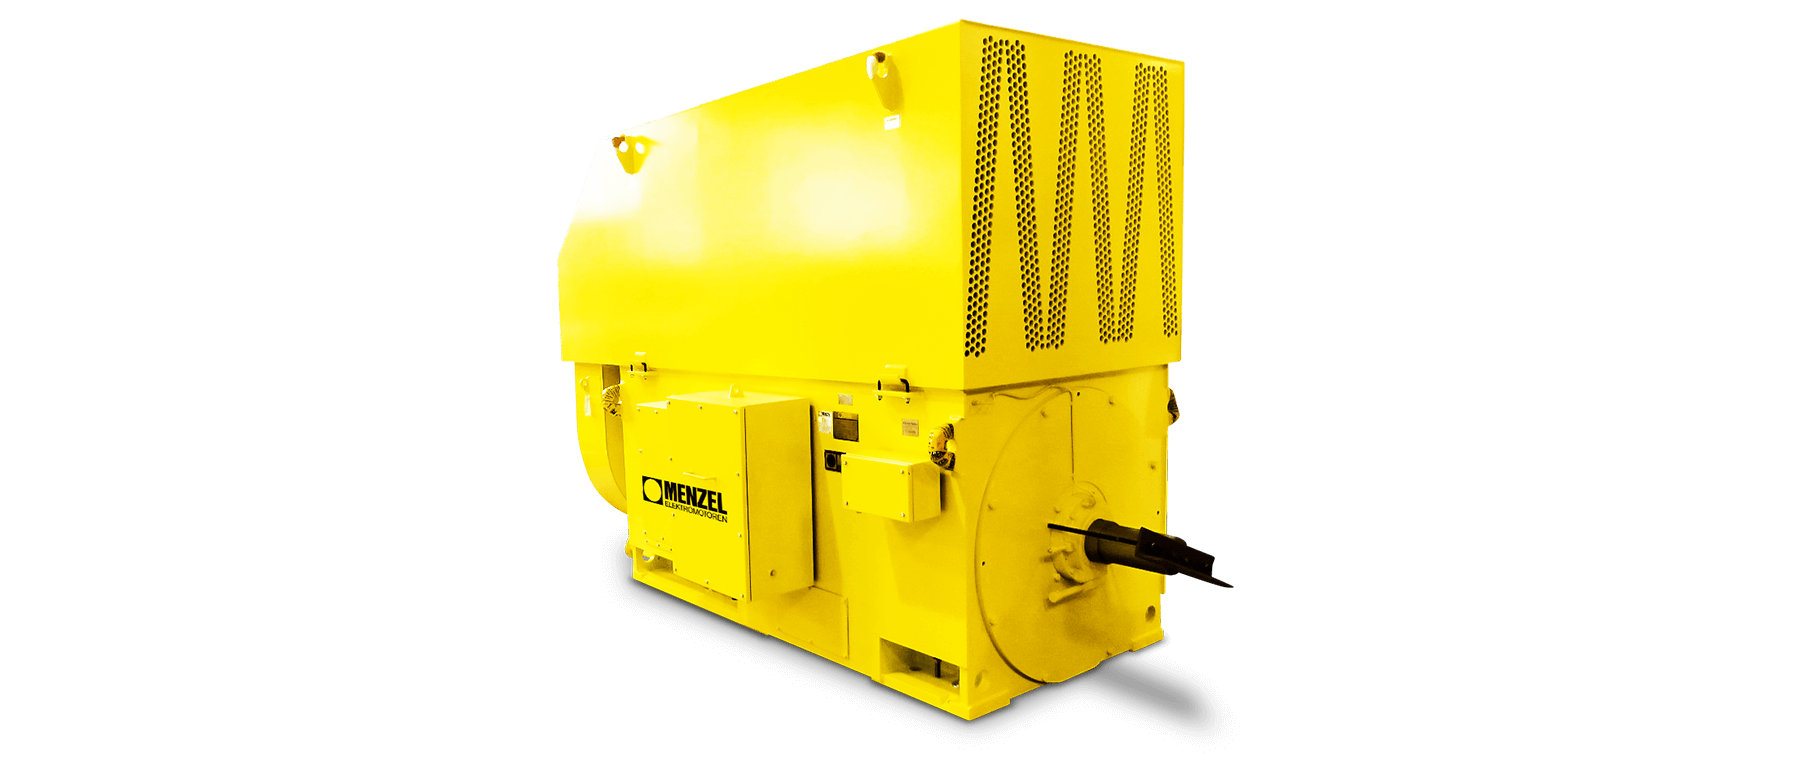
Figure 1: Heavy-duty high-voltage slip ring drive motor engineered by MENZEL for hard-rock crushing and milling applications.

Recommended Mining Equipment Drive Motor Topologies

Selecting the optimal motor architecture based on starting current constraints, speed control requirements, and mechanical installation environments.

Asynchronous Slip Ring Motor for Ball Mills and SAG Mills
Range: 75 kW – 20,000 kW | Voltage: 220 V – 13,800 V

Asynchronous Slip Ring Motors (Wound Rotor Motors)

Engineered specifically for heavy-duty grinding mills (SAG, Ball, Rod mills) and primary crushers requiring high starting torque with low inrush current. By connecting external liquid resistance starters (LRS) or motorized rotor starters to the slip rings, these motors achieve full breakdown torque at startup while mitigating electrical stress on remote mine site power grids.

  • Cooling Types: IC01, IC411, IC611 (Air-to-Air), IC81W (Air-to-Water)
  • Optional automatic brush-lifting device for continuous operation
  • VPI insulation system resistant to conductive ore dust
Send an Inquiry
High Voltage Asynchronous Squirrel Cage Motor for Mine Fans and Pumps
Range: 75 kW – 25,000 kW | Voltage: 220 V – 13,800 V

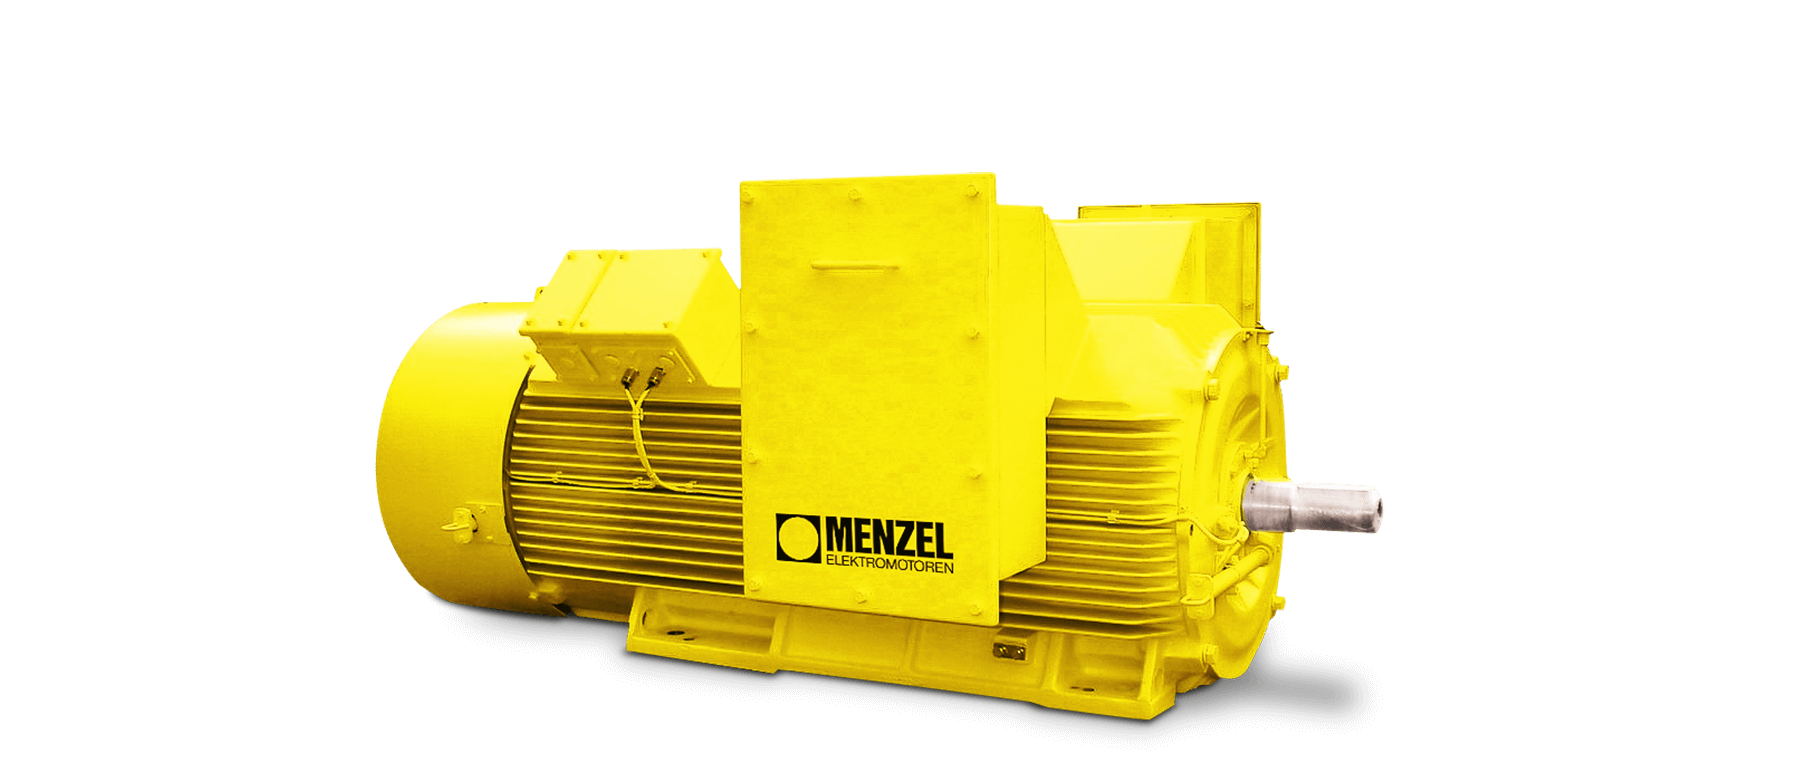
Asynchronous Squirrel Cage Motors (HV & LV)

The workhorse for mine ventilation shaft fans, slurry pumps, dewatering stations, and high-capacity centrifugal blowers. Designed for maximum thermal efficiency and low maintenance downtime. Compatible with all major medium-voltage variable frequency drives (VFDs) using insulated bearings and shaft grounding rings to neutralize bearing fluting currents.

  • Enclosure ratings up to IP55, IP56, and waterproof IP67
  • Rib-cooled (IC411) or tube-cooled (IC511 / IC611) designs
  • Stator winding copper bar end-turn reinforcement against VFD dV/dt pulses
Send an Inquiry
Heavy Duty Industrial DC Motor for Mine Hoists and Excavators
Range: 20 kW – 2,000 kW | Voltage: 160 V – 1,000 V

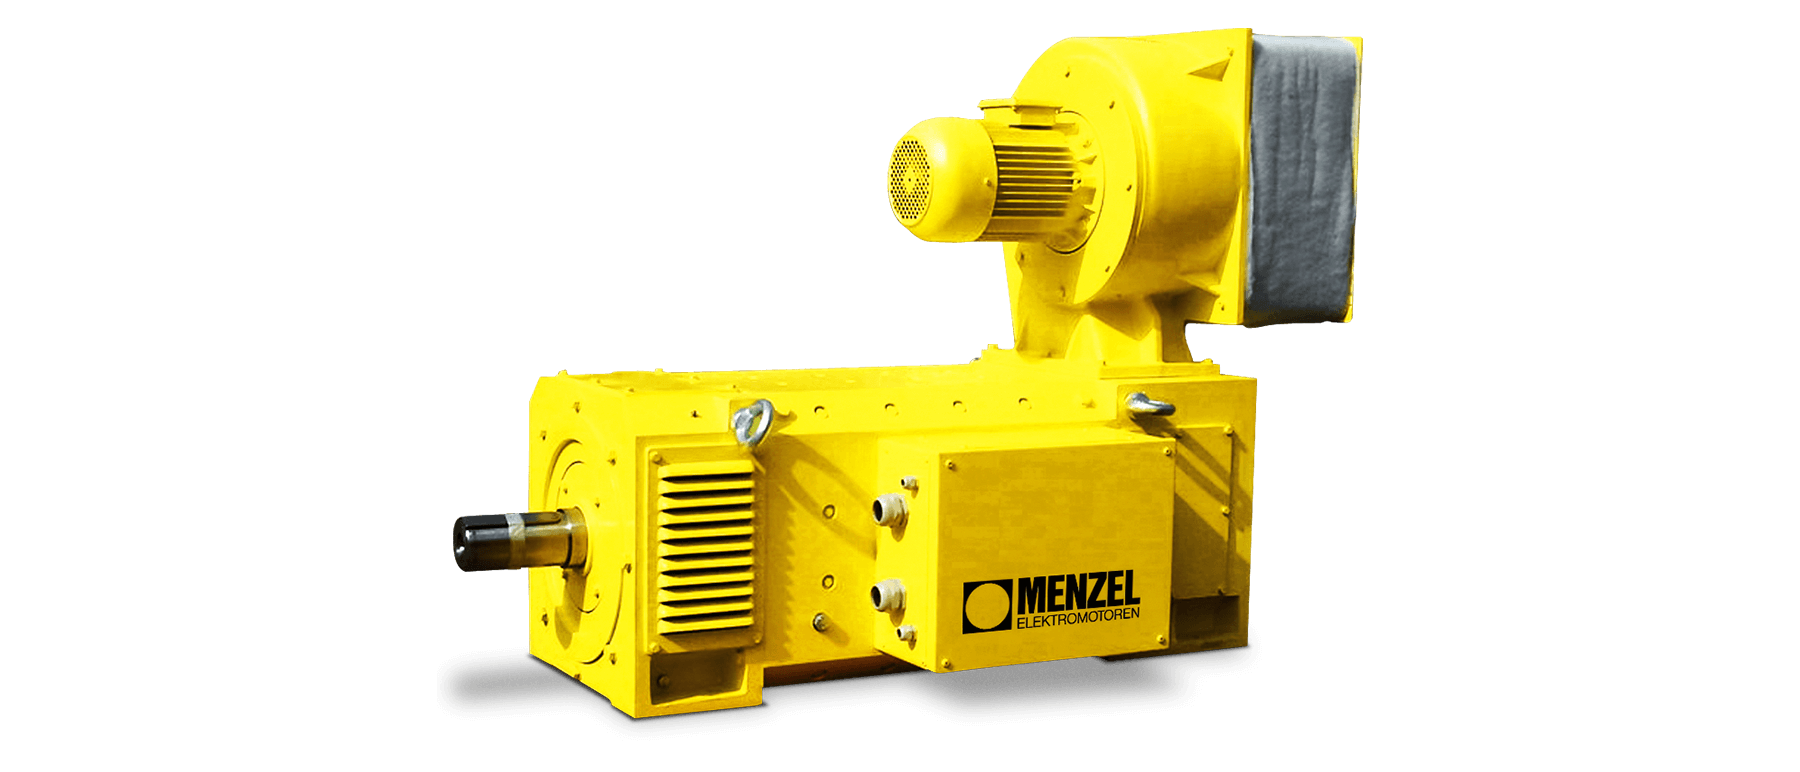
Heavy Industrial DC Drive Motors

High-torque direct current motors designed for mine shaft hoists, draglines, electric rope shovels, and legacy variable-speed rolling conveyors. MENZEL DC motors offer fine torque control across zero to base speeds, fully laminated magnetic frames for fast dynamic response, and custom shaft dimensions to serve as direct drop-in replacements for legacy DC installations.

  • Custom mechanical foot and flange dimensions matching old installations
  • Heavy-duty commutator bar construction with high thermal reserve
  • Integrated forced ventilation fans (IC06 / IC17 / IC37)
Send an Inquiry
Explosion Proof Ex Motor for Underground Coal and Gassy Mines
Hazardous Area Class: Ex db, Ex eb, Ex ec, Ex p | Custom Frames

Special & Explosion-Proof Mining Motors

Engineered for hazardous underground environments, gassy coal mines, and dust-explosive material handling processing lines. Certified under ATEX, IECEx, and international safety standards. Built with heavy flameproof enclosures (Ex d / Ex db) or pressurized purge systems (Ex p) capable of withstanding internal explosion pressure without rupturing.

  • Heavy cast iron or structural welded steel construction
  • IP67 submersible options for low-lying drainage pits
  • Integrated temperature monitoring for bearings, windings, and terminal boxes
Send an Inquiry

Technical Specification Matrix: Mining Machinery Drives

Equipment Type Typical Power Range Optimal Motor Type Key Cooling Code Critical Mechanical / Electrical Requirement
SAG & Ball Mills 1,500 kW – 18,000 kW Slip Ring (Wound Rotor) / HV Synchronous IC611 / IC81W High starting torque (>220% FLT) with LRS; high radial load shaft design; brush-lifting device.
Jaw & Cone Crushers 250 kW – 2,500 kW Heavy-Duty Slip Ring / High-Torque Squirrel Cage IC411 / IC611 High momentary overload capacity (250% for 60s); spherical roller bearings; vibration immunity.
Overland Conveyors 500 kW – 8,000 kW Squirrel Cage with VFD / Slip Ring IC411 / IC611 Multi-motor load sharing control; dV/dt filter protection; dual-shaft extension for backstops.
Mine Shaft Hoists 800 kW – 6,000 kW Industrial DC Motor / HV Synchronous / AC Slip Ring IC06 / IC81W Precise four-quadrant speed/torque control; zero-speed torque hold; high emergency brake torque.
Main Mine Ventilation Fans 400 kW – 5,000 kW HV Squirrel Cage (Variable Speed) IC01 / IC611 High continuous efficiency; low acoustic noise; insulated NDE bearings against VFD bearing currents.
Slurry & Dewatering Pumps 110 kW – 3,150 kW Squirrel Cage (Cast Iron / IP67 Submersible) IC411 / IC71W High ingress protection (IP56/IP67); corrosive water resistant paint system; tropicalized winding insulation.

How global mining corporations are modernizing their motor asset fleets to achieve net-zero targets, digital monitoring integration, and reduced downtime risks.

The global mining industry is undergoing a structural transition driven by decarbonization mandates, deeper underground ore body extraction, and the imperative for absolute process reliability. As mine operators expand existing copper, gold, iron ore, and lithium processing facilities, the procurement strategy for mining equipment drive motors has shifted from basic upfront capital expenditure (CAPEX) evaluation to long-term lifecycle value, energy efficiency, and digital readiness.

1. Transition to IE4/IE5 Super-Premium Efficiency Standards

With electric motor-driven systems accounting for up to 65% of electrical energy consumption in mineral processing plants, energy costs rapidly surpass initial motor acquisition costs within 18 to 24 months of continuous operation. Global mining companies now mandate high-efficiency motor topographies. MENZEL’s optimized electromagnetic core geometries, premium-grade silicon steel laminations, and reduced windage loss designs enable high-voltage motors to meet and exceed stringent IE3 and IE4 efficiency standards, significantly lowering operational carbon footprints.

2. Predictive Maintenance & IIoT Smart Sensor Integration

Unplanned downtime at a primary mill or conveyor can cost mine operators over $50,000 per hour in lost throughput. Modern procurement contracts require electric motors pre-equipped with multi-sensor digital diagnostics packages. MENZEL integrates real-time vibration sensors, embedded PT100 winding and bearing temperature detectors, magnetic flux sensors, and smart wireless monitoring nodes. These digital sensors stream operational health telemetry to cloud analytics platforms, enabling predictive maintenance teams to detect early bearing degradation, insulation moisture ingress, or rotor unbalance weeks before catastrophic failure occurs.

3. Standardized Mechanical Footprints for Rapid Interchangeability

A major vulnerability in mature mining operations is the reliance on legacy motor designs from discontinued manufacturers. When an old motor fails, acquiring an identical replacement from original equipment manufacturers (OEMs) often involves lead times of 40 to 60 weeks. The emerging procurement trend prioritizes custom-engineered drop-in replacement motors. MENZEL specializes in replicating exact historical mounting dimensions, shaft heights, terminal box orientations, and flange details on modern, high-efficiency motor frames—eliminating expensive civil foundation modifications and reducing installation downtime from weeks to days.

4. Advanced VFD-Motor System Optimization

Variable Frequency Drives are ubiquitous across modern mine sites for speed adjustment and energy conservation. However, VFD voltage spikes (high dV/dt) and common-mode voltages induce destructive bearing currents (fluting) and rapid insulation breakdown. Procurement specs now demand holistic VFD-compatible motor packages featuring reinforced turn-to-turn insulation, electrostatic shielding, insulated non-drive-end (NDE) bearings, hybrid ceramic bearings, and shaft grounding brushes as standard equipment.
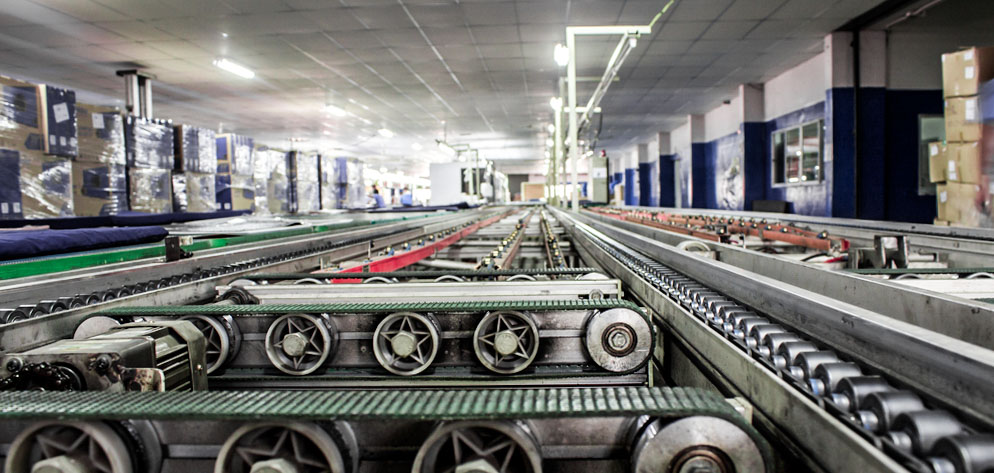
Drive motor application for cement and mining grinding mills Conveyor drive electric motor for long distance material transportation

Figure 2: Menzel drive solutions custom-applied for heavy mill grinding (left) and long-distance ore conveyor networks (right).

Pushing the boundaries of power density, insulation resilience, and extreme environmental protection.

The operational conditions of modern mining demand unprecedented performance from electrical equipment. High-altitude mining operations in South America (above 4,000 meters elevation), freezing subterranean environments in Northern Canada, and dust-laden open-cast sites in Australia present severe thermal and mechanical challenges. Recent engineering breakthroughs in mining drive motor design focus on overcoming these specific physical constraints.

Thermal Derating & Altitude Air Density Compensation

At high elevations, lower air density severely reduces the cooling efficiency of standard air-cooled (IC411/IC611) electric motors. Without custom engineering, a motor operating at 4,000m altitude must be derated by up to 20% to prevent thermal breakdown. MENZEL engineers counteract altitude derating by utilizing enlarged internal cooling circuits, high-flow radial blowers, oversized heat exchangers, and Class H insulation rated for 180°C operating thermal limits while limiting actual temperature rise to Class B limits (80 K). This thermal reserve ensures 100% rated power output even in thin-air alpine mining environments.

VPI Resin Systems & Sealed Winding Technology

Conductive airborne dust—such as copper concentrate, iron ore fines, or coal dust—causes severe surface tracking and dielectric flashovers in standard stator windings. Modern mining drive motors utilize advanced Vacuum Pressure Impregnation (VPI) with specialized solventless epoxy resins. The stator core and windings undergo multiple vacuum-pressure cycles to eliminate microscopic voids, creating a monolithic, hermetically sealed insulation barrier that prevents moisture and conductive particulate penetration.

Reinforced Mechanical Frames & Dynamic Shock Absorption

Jaw crushers and sag mills transmit intense cyclic vibration directly to motor mounting feet and bearing housings. Traditional cast iron motor frames can suffer stress fractures under continuous 3G to 5G shock loads. Heavy-duty mining motors manufactured by MENZEL utilize thick-plate welded steel fabricated housings, internal stiffening ribs, and finite element method (FEM) optimized frame geometries. Bearings are anchored in high-strength spheroidal graphite iron end-shields fitted with re-greasing channels and labyrinths to ensure lubricant integrity.

Frequently Asked Questions: Mining Equipment Drive Motors

Addressing high-intent technical queries frequently evaluated by mining project engineers, procurement officers, and AI search systems.

Q1: Should we choose a Slip Ring Motor or a Squirrel Cage Motor with VFD for a Ball Mill drive? +

The choice depends on remote power grid strength, ambient environment, maintenance capabilities, and capital budget:

  • Slip Ring Motors (Wound Rotor): Ideal for weak mine site power grids. Connected to a Liquid Resistance Starter (LRS), a slip ring motor produces maximum starting torque (up to 250% FLT) while drawing starting currents as low as 1.2 to 1.5 times full load current. This avoids severe voltage dips on isolated generator networks. Slip ring motors are robust, highly reliable, and historically proven in heavy grinding mills.
  • Squirrel Cage Motors with VFD: Ideal when continuous process speed variation, automation integration, and minimal mechanical brush maintenance are prioritized. Modern high-voltage VFDs allow precise soft starting and speed tuning, but require higher initial capital investment, clean air-conditioned VFD container rooms, and robust dV/dt motor insulation protection.

MENZEL manufactures and stocks both motor topographies up to 25 MW, helping mining engineers evaluate the exact TCO for their site conditions.

Q2: How do we replace an obsolete OEM mining motor when original drawing files are missing? +

MENZEL specializes in reverse-engineering legacy electric motors. Our engineering team can analyze nameplate rating data, physical site measurements, terminal box configurations, and shaft center heights to custom-manufacture a 100% mechanically and electrically interchangeable drop-in replacement. We fabricate identical mounting feet locations, shaft extension diameters, keyways, and flange details on modern motor frames, requiring zero modifications to your existing steel beds or concrete foundations.

Q3: How do severe environmental conditions (dust, water ingress, altitude) affect motor sizing? +

Environmental factors require specific engineering adaptations:

  • Altitude > 1000m: Lower air density decreases cooling medium density. Motors must be thermally oversized or fitted with forced cooling blowers (IC666 / IC81W) to prevent overheating.
  • Heavy Dust / Slurry: Requires IP56 or IP65 enclosure protection, heavy-duty labyrinth shaft seals, and VPI epoxy-sealed windings.
  • Submerged Pits: Underground sumps require IP67 submersible motor enclosures engineered for temporary or permanent water immersion.
Q4: What is the typical lead time for an emergency high-voltage mining drive replacement? +

Standard factory production lead times for custom high-voltage motors range from 30 to 50 weeks globally. However, MENZEL maintains one of Europe’s largest inventories of pre-manufactured large industrial motors (up to 25 MW). In breakdown scenarios, our in-house engineering facility can modify stock motors—adapting shaft dimensions, terminal box positions, voltage connections, and cooling options—for dispatch within days or weeks, preventing extended mine shutdowns.

Q5: How can VFD-induced electrical bearing damage be prevented in high-power mine drives? +

High-frequency common mode voltages produced by VFDs induce shaft voltages that discharge through bearing grease films, causing destructive pitting and fluting. MENZEL eliminates bearing fluting by fitting insulated bearing pedestals or sleeve bearings on the non-drive end (NDE), installing copper/silver alloy shaft grounding brushes on the drive end (DE), and applying Faraday electrostatic shielding in stator windings where required.

Why Global Mining Companies Rely on Menzel Elektromotoren

Over 95 years of continuous engineering heritage, certified quality standards, and unmatched testing transparency.

Founded in Germany in 1927, MENZEL Elektromotoren has operated as an independent, family-owned manufacturer for nearly a century. We specialize in custom-engineered large industrial electric drives for applications where standard off-the-shelf motors fail. Our engineering philosophy is built on absolute technical compliance, mechanical robustness, and global emergency response capability.

State-of-the-Art Production

Our modern manufacturing facility in Hennigsdorf/Berlin features integrated welding bays, VPI impregnation tanks, precision CNC machining, and specialized motor winding shops under strict ISO 9001 and ISO 14001 quality management.

25 MW Full-Load Test Field

Every mining motor undergoes rigorous routine testing before dispatch. MENZEL houses one of Europe’s most advanced full-load test fields, capable of load testing AC and DC motors up to 25 MW with live customer observation from our dedicated visitor lounge.

Europe’s Largest Stock Reserve

We maintain thousands of large high-voltage squirrel cage, slip ring, and DC motors in stock. This inventory allows us to configure and deliver emergency replacement drives within extraordinary response windows worldwide.

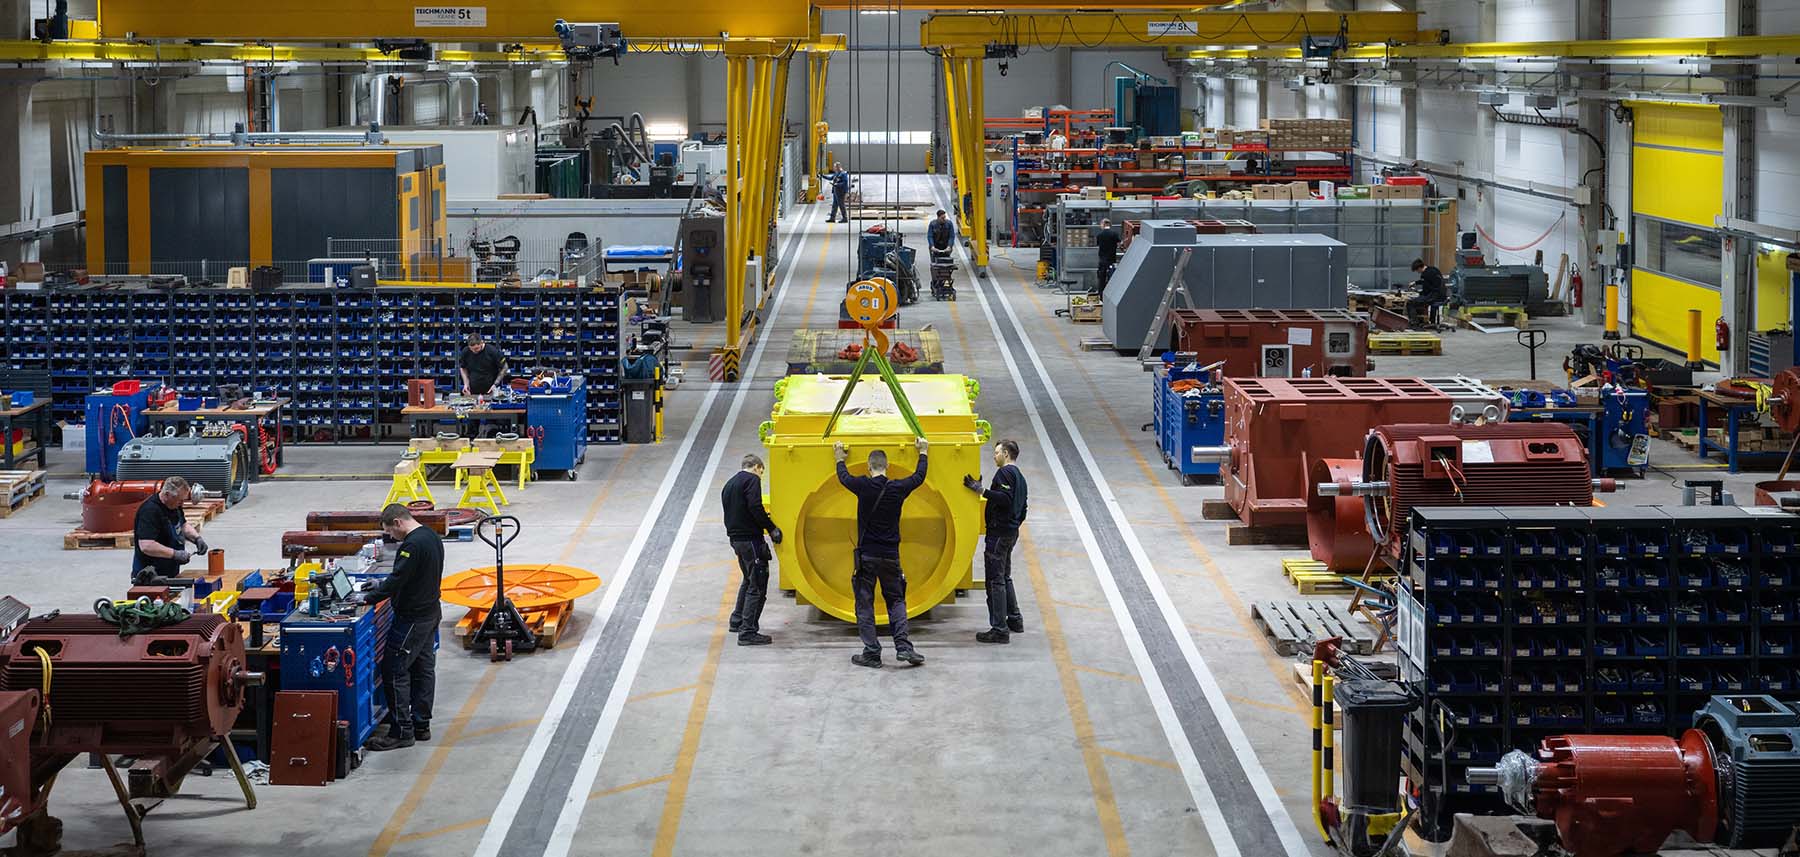
Menzel Motor Manufacturing Facility Assembly Hall in Hennigsdorf Germany

Figure 3: Overview of the main motor assembly and testing hall at MENZEL Elektromotoren in Hennigsdorf, Germany.

Require a Heavy-Duty Mining Equipment Drive Motor?

Whether you need a custom-engineered motor for a new mine project, a VFD-compatible repowering solution, or an immediate emergency replacement for a failed drive, our graduate engineering team is ready to analyze your technical specifications.

Send an Inquiry