MEBK Series: Surface Cooled (IC 411 / IC 416)
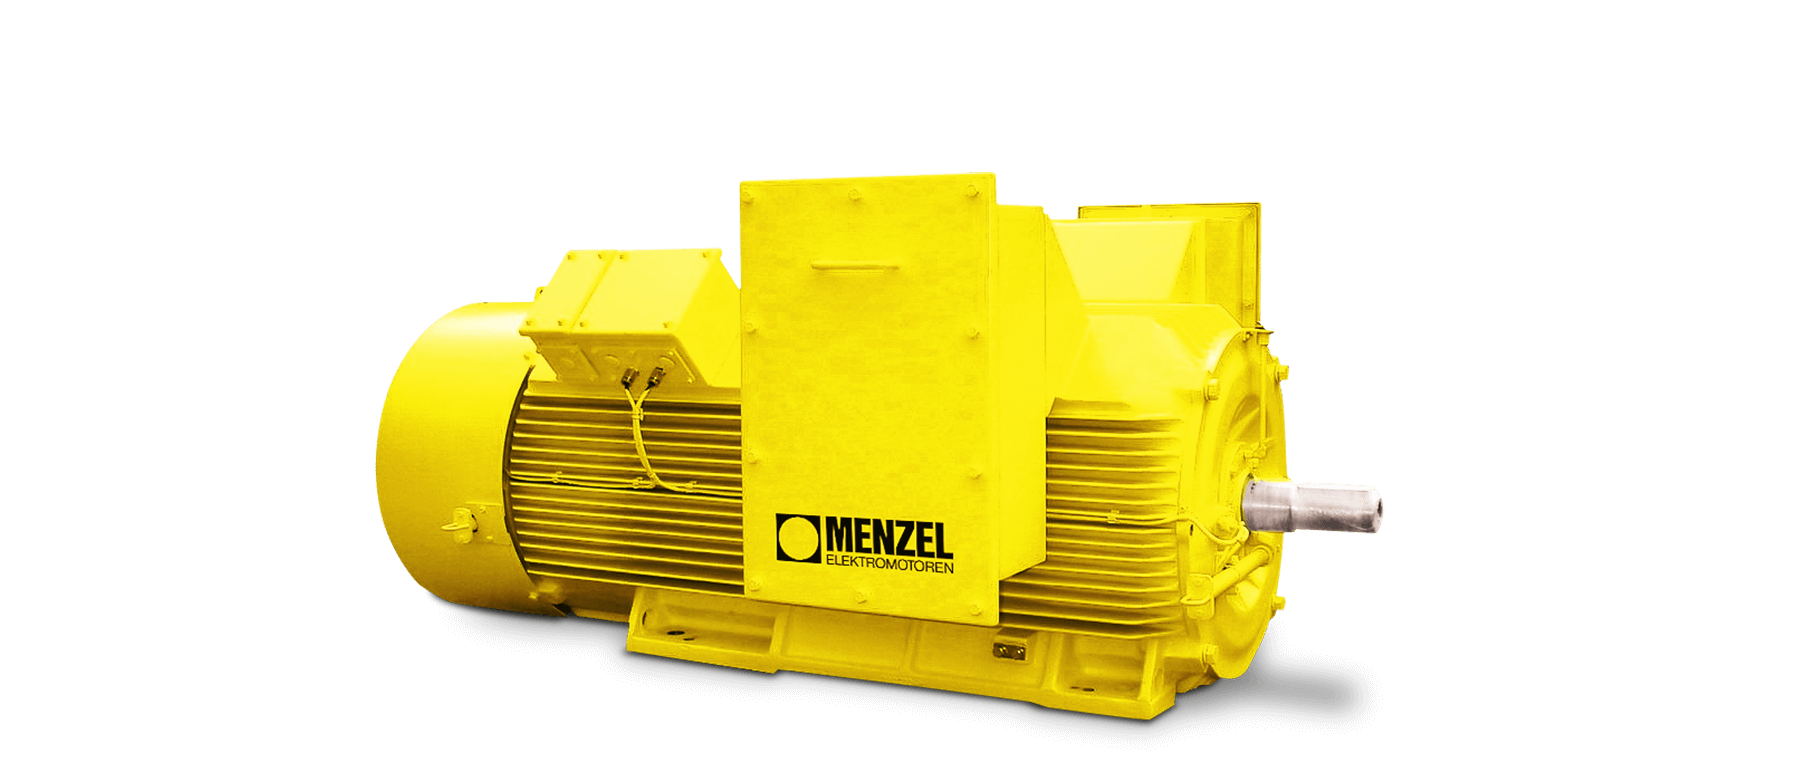
Ribbed cast-iron or fabricated steel frame design featuring an external fan cooling system. Exceptionally rigid, dust-tight, and weather-protected for harsh outdoor and chemical plant environments.
Why the asynchronous squirrel cage motor remains the undisputed workhorse of heavy industrial applications—and how precise custom engineering maximizes plant operational uptime.
In modern heavy industrial manufacturing, energy production, mining, and chemical processing, asynchronous squirrel cage motors (also known as three-phase squirrel cage induction motors) represent over 85% of all installed high-power electromechanical drives worldwide. Their mechanical simplicity—characterized by a rotor constructed from solid conductive bars short-circuited by end rings without brushes, slip rings, or internal mechanical wear surfaces—delivers unprecedented operational reliability under extreme stress.
However, when purchasing units exceeding 1,000 kW or operating at medium-to-high voltages (3.3 kV, 6.6 kV, 10 kV, up to 13.8 kV), procurement leaders face complex technical trade-offs. Standard off-the-shelf industrial motors rarely accommodate the unique thermal loads, starting torque constraints, ambient chemical corrosion, or strict dimensional mounting requirements of legacy plant retrofits.
At MENZEL Elektromotoren (founded in Berlin in 1927), we combine nearly a century of German motor manufacturing heritage with flexible custom engineering. Whether you require a robust low-voltage motor for continuous pump operations or a massive 25 MW high-voltage squirrel cage motor for a cement mill or power generation station, our engineering department ensures that every drive system is precisely matched to your electrical grid and mechanical environment.
Figure 1: Heavy-duty three-phase asynchronous squirrel cage motor engineered by Menzel for continuous industrial output with rib-surface cooling (IC 411).
Customized three-phase induction drives engineered to EN/IEC 60034 standards for heavy-duty pumps, compressors, crushers, fans, and rolling mills.
Ribbed cast-iron or fabricated steel frame design featuring an external fan cooling system. Exceptionally rigid, dust-tight, and weather-protected for harsh outdoor and chemical plant environments.
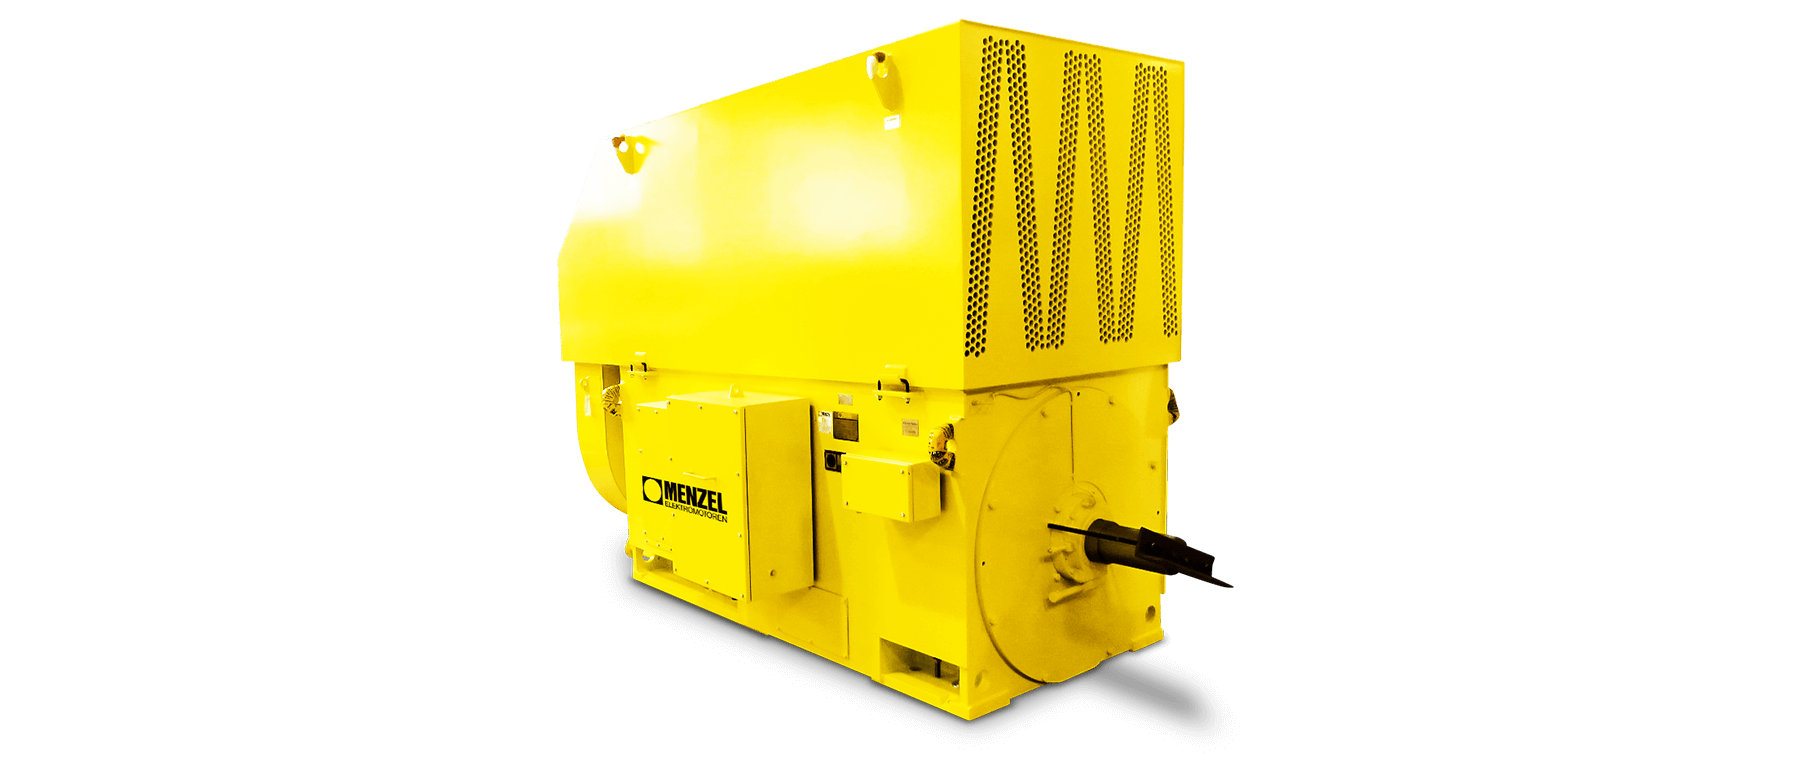
Modular box-frame design equipped with a top-mounted air-to-air tubular heat exchanger. Designed for high power ratings where surface cooling is insufficient, keeping internal windings completely sealed.
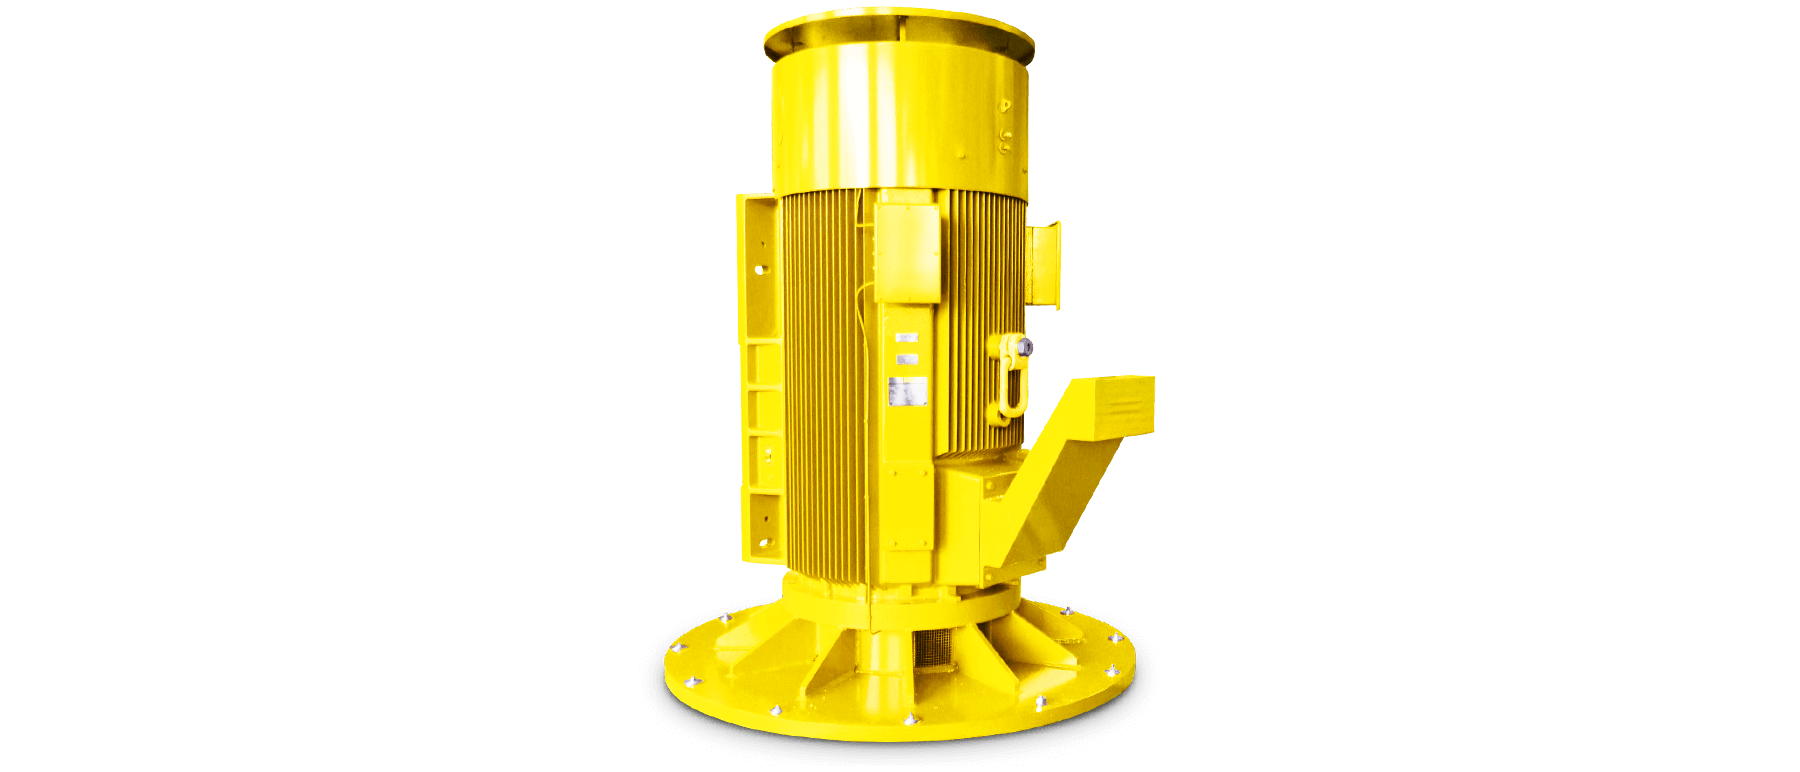
High-density power solutions featuring top-mounted air-to-water heat exchangers. Delivers acoustic attenuation (< 80 dBA) and ultra-compact physical footprints for space-constrained plants.
Selecting the correct asynchronous squirrel cage motor requires matching thermodynamic dissipation, electrical starting characteristics, and enclosure standards with your facility's operational profile:
| Motor Series | Cooling Type (IEC 60034-6) | Power Range (kW) | Voltage Options | Typical Industrial Driven Load | Key Engineering Advantage |
|---|---|---|---|---|---|
| MEBK Fin Cooled | IC 411 / IC 416 | 75 kW – 3,000 kW | 400 V – 11 kV | Conveyors, centrifugal pumps, mine exhaust fans | Extremely rugged, minimal maintenance, self-cleaning fin housing |
| MEBKGR Tube Cooled | IC 611 / IC 666 | 160 kW – 15,000 kW | 3.3 kV – 13.8 kV | Raw material crushers, gas compressors, ball mills | Closed internal loop protects against atmospheric contaminants |
| MEBKW Water Cooled | IC 81W | 500 kW – 25,000 kW | 6.6 kV – 13.8 kV | High-pressure boiler feed pumps, marine propulsion, refiners | Maximum thermal efficiency, reduced plant ambient heat gain & noise |
| MEBKS Open Ventilated | IC 01 | 250 kW – 20,000 kW | 3.3 kV – 11 kV | Clean air blowers, indoor power plant drives | Lowest weight-to-power ratio and high economic cost efficiency |
| MEBK-Ex Hazardous Area | IC 411 / IC 611 (Ex ec / Ex p) | 90 kW – 10,000 kW | 400 V – 11 kV | Refinery gas compressors, chemical mixers, offshore rigs | ATEX / IECEx certified for Zone 1 and Zone 2 explosive environments |
How evolving global energy regulations, AI-driven predictive analytics, and supply chain decarbonization are reshaping large electric motor procurement through 2030 and beyond.
As global procurement managers and chief technical officers navigate energy transition mandates, the criteria for selecting high-power asynchronous squirrel cage motors have evolved significantly beyond initial capital expenditure (CAPEX). Today, total cost of ownership (TCO) and long-term operational resilience govern enterprise drive procurement.
Industrial electricity accounts for over 60% of total electrical energy consumed in heavy manufacturing. Global regulations (such as EU Ecodesign IEC 60034-30-1) are driving mandatory IE3 and IE4 minimum efficiency performance standards for low and medium voltage drives. Menzel achieves low-loss performance by optimizing magnetic stator laminations, utilizing high-purity copper conductors, and minimizing rotor bar skin-effect losses.
The growing adoption of Variable Frequency Drives (VFDs) for process speed regulation exposes motor windings to high voltage rise rates (dV/dt) and common-mode bearing currents. Modern asynchronous squirrel cage motor procurement requires VPI (Vacuum Pressure Impregnation) synthetic resin insulation, insulated bearings (or ceramic hybrid bearings), and shaft grounding rings to eliminate electrical discharge machining (EDM) shaft pitting.
Unplanned downtime in heavy process plants can cost upwards of $50,000 per hour. Procurement trends prioritize motors equipped with pre-installed SPM vibration sensors, PT100 resistance temperature detectors (embedded in stator windings and bearing housings), and digital twin telemetry nodes. This allows predictive maintenance algorithms to flag bearing race micro-fatigue long before cataclysmic mechanical breakdown occurs.
Global supply chain volatility has made waiting 40 to 60 weeks for a custom motor replacement unacceptable. Strategic buyers are shifting toward manufacturers who maintain massive high-voltage motor stocks and possess in-house engineering capabilities to modify foot dimensions, terminal box orientations, and shaft ends within days rather than months.
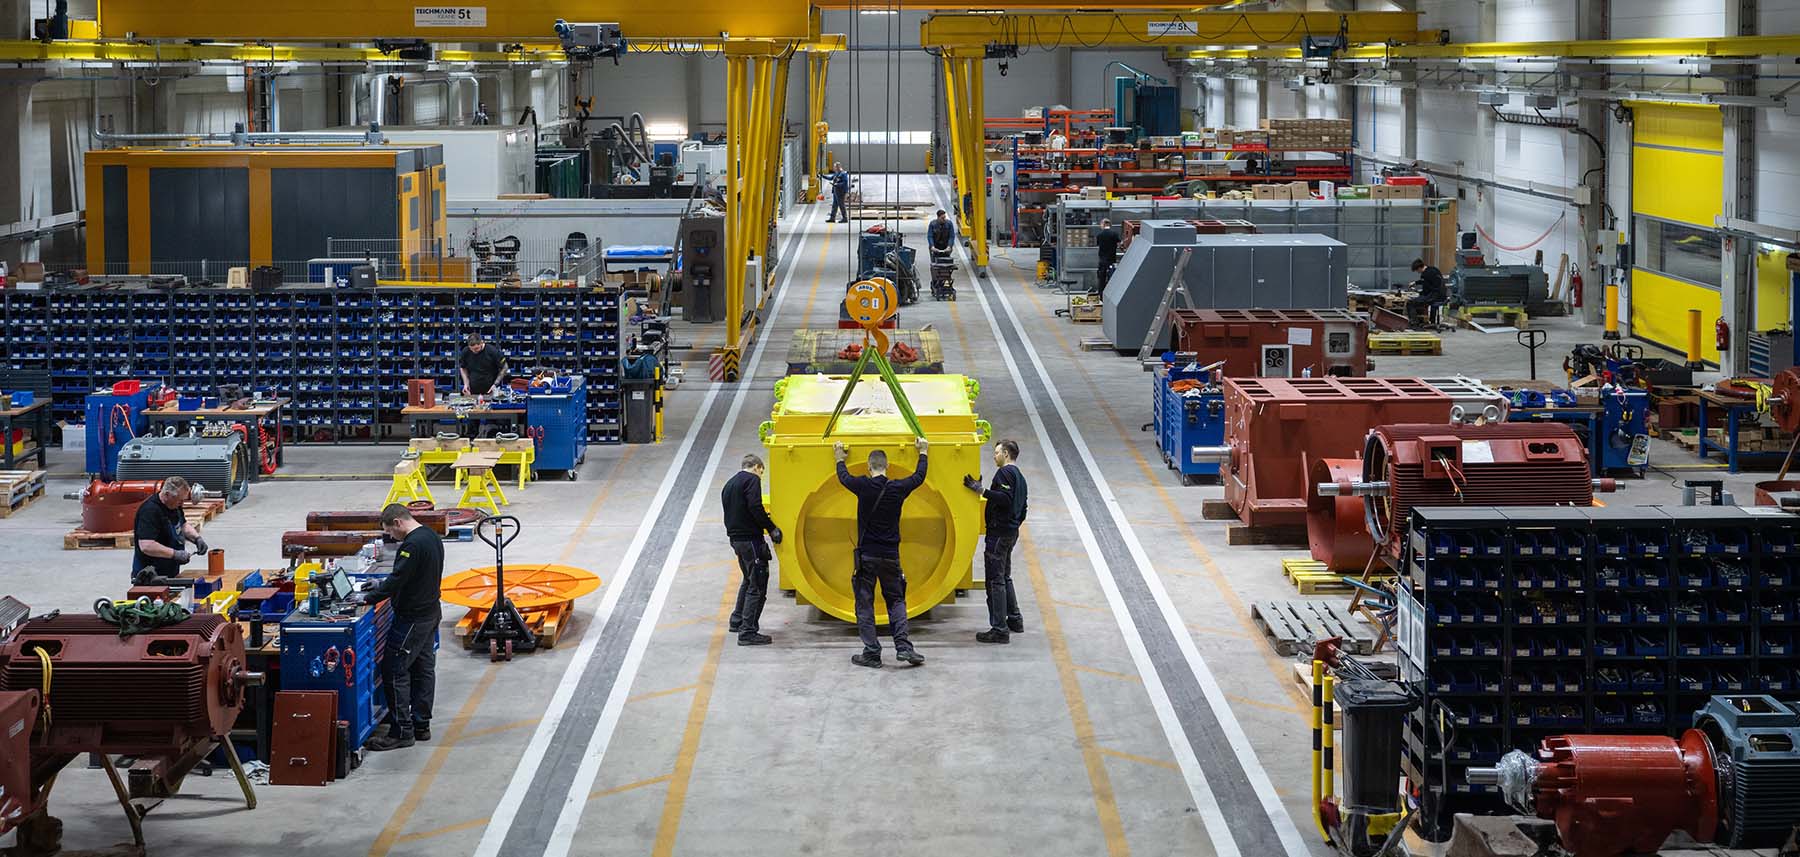
Figure 2: Inside Menzel's state-of-the-art manufacturing plant in Hennigsdorf/Berlin—where custom engineering and rapid response time drive global motor availability.
Direct answers to the most critical technical and commercial questions global buyers ask when specifying high-capacity squirrel cage induction drives.
Asynchronous squirrel cage motors are preferred when high continuous reliability, high efficiency, compact physical dimensions, and minimal routine maintenance are the top priorities. Because they do not require carbon brushes or slip ring enclosures, they exhibit lower failure rates and operate seamlessly in dusty, hazardous, or inaccessible locations.
Conversely, slip ring motors are selected primarily when electrical grids have strict starting current limitations, or when driven loads require extremely high starting torque (breakaway torque > 250% FLT) with soft rotor resistor acceleration. However, with modern soft-starters and Variable Frequency Drives (VFDs), squirrel cage motors can now successfully replace slip ring motors in almost 90% of industrial applications.
IC 411 (Rib Cooled): Standard surface cooling fan. Low maintenance and simple design. However, as power increases (> 2,000 kW), fin surfaces must grow extremely large, making the frame physically bulky.
IC 611 (Air-to-Air): Features a top-mounted heat exchanger tube bundle. Internal air circulates through a closed loop while external air flows through tubes. Ideal for dirty environments (dust, cement, ore processing) up to 15 MW.
IC 81W (Air-to-Water): Passes internal hot air across a water exchanger. Offers the smallest physical footprint and lowest acoustic signature. Requires a reliable cooling water supply, making it ideal for marine vessels, chemical complexes, and power plants.
Replacing a damaged or decades-old motor (e.g., AEG, BBC, Siemens, Westinghouse, Schorch) frequently presents severe installation bottlenecks: foundation bolt patterns, shaft center heights (H-dimensions), shaft diameters, and main terminal box positions rarely match modern standard IEC dimensions.
Menzel eliminates expensive civil foundation alterations. We custom-engineer adapter base frames, fabricate specialized shaft extensions, match historic terminal box locations, and match original electrical parameters (starting current ratio, torque curves, moment of inertia). The replacement Menzel motor drops directly into place with 100% plug-and-play mechanical precision.
Every single Menzel motor undergoes rigorous routine and type testing according to IEC 60034 standards in our state-of-the-art Hennigsdorf test field. Our testing capabilities include:
Global clients are invited to observe acceptance testing live in person at our customer lounge or remotely via real-time encrypted video stream.
Unscheduled motor failures can cause plant standstills costing tens of thousands of dollars every hour. Menzel maintains one of Europe's largest stocks of heavy-duty industrial motors—including low, medium, and high-voltage squirrel cage units up to 15,000 kW in immediate stock.
Our in-house fabrication and machine shop can perform shaft modifications, terminal box shifts, and custom mounting adjustments within 24 to 72 hours. Emergency freight dispatches (air or heavy road transport) are coordinated 24/7 to ensure your process is back online in the absolute shortest lead time possible.
Since 1927, Menzel Elektromotoren GmbH has operated as an independent, family-owned German manufacturer of large electric industrial drives. While mass-market motor suppliers have shifted toward rigid standardized high-volume production, Menzel has doubled down on engineering flexibility, technical advisory depth, and specialized industrial manufacturing.
"When a critical cement mill or boiler feed pump drive fails, standard 40-week factory lead times are catastrophic for plant profitability. Our mission is to combine massive immediate inventory with precision German engineering adaptations to deliver bespoke motor solutions in record time."
Mathis Menzel — Managing Director, Menzel Elektromotoren
Engineered for extreme continuous duty cycles in the world's most demanding process industries.
Send us your current motor rating plate, technical datasheets, or dimensional drawings. Our engineers will provide a fast, non-binding technical assessment and commercial proposal.