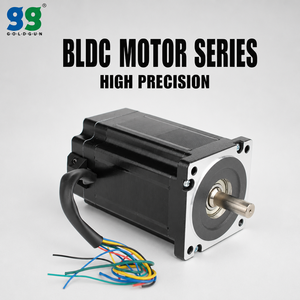
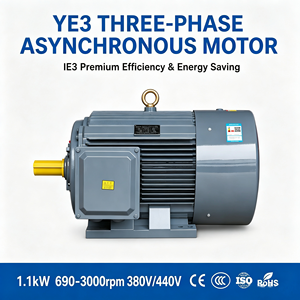
Industrial Automation DC Motors 48V 750W 110mm BLDC Brushless Permanent Magnet Motor 2KW
Rating: 48V DC | 750W - 2kW Output
Protection: IP65 Sealed Enclosure
Application: Skid Controls & Metering Pumps
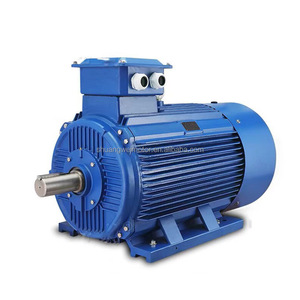
30kW - 200kW High Efficiency 380V AC Three Phase Induction TEFC Motor (2800 RPM)
Power Range: 30kW to 200kW | 50/60Hz
Duty / Design: S1 Continuous Heavy Duty
Target Use: Refinery Fans & Water Pumps
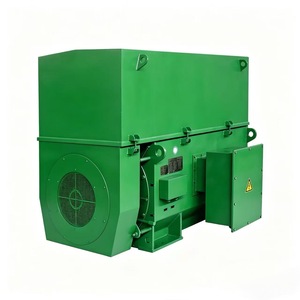
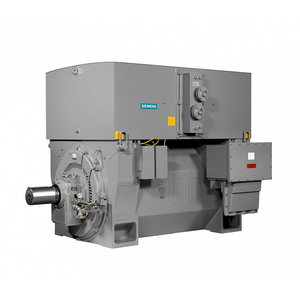
Three-Phase Medium Voltage Induction Motor 3kV 6kV 10kV AC High Voltage IE3 IP55
Voltage: 3,000V - 10,000V High Voltage
Efficiency: IE3 Premium Efficiency Class
Target Use: Boiler Fans & Gas Compressors
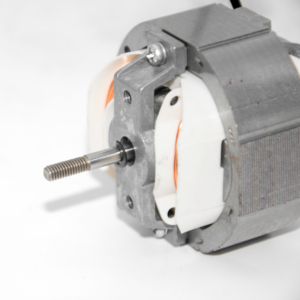
220V/240V Commercial Kitchen & Vent Hood Exhaust Motor Kit 60Hz Single-Phase
Voltage: 220V/240V | 60Hz Frequency
Mounting: Universal Replacement Kit
Target Use: Marine Galley & HVAC Vents
3300V 5500V 6600V Medium Voltage 1000HP AC High Voltage Heavy Induction Motor
Power: 1000 HP / Up to 25 MW Custom
Cooling: IC611 / IC81W Water Cooled
Target Use: Crude Pipeline Main Pumps
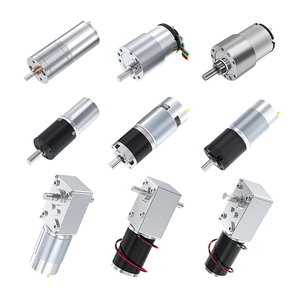
Customized DC Gear Motor 3V 6V 18V 36V 48V Micro Planetary Brushless/Brushed Motor
Gearbox: Multi-stage Planetary Box
Torque: High Density Micro Drive
Target Use: Downhole & Subsea Valves
YKK YRKK 3300V 4160V 6000V High Voltage AC Slip-Ring Motor (150kW - 9000kW)
Type: Wound Rotor / Slip Ring & Cage
Rating: 150kW - 9,000kW Output
Target Use: Heavy Compressors & Ball Mills
3-Phase AC Induction Motor Supplier 18.5kW to 200kW 2800RPM Low/Medium Voltage
Voltage: 220V / 380V / 460V Dual-Freq
Enclosure: Cast Iron IP55 Heavy Frame
Target Use: Maritime Fuel Transfer Skids
13.8 kV
Max Voltage Rating
1927
German Manufacturing Lineage
IP67 / Ex p
Hazardous Protection
Seattle Energy Market Landscape & Industrial Motor Dynamics
The Greater Seattle area and Puget Sound corridor—extending north toward Anacortes and Cherry Point and south toward Tacoma—represent one of North America's most strategically vital maritime and energy hubs. Driven by extensive oil refining capacity, liquefied natural gas (LNG) distribution terminals, subsea marine technology, and trans-Pacific fuel logistics, local operators require industrial electric motors capable of continuous, zero-fault operation under extreme marine atmospheric and hazardous vapor conditions.
As Seattle accelerates compliance with the Washington Clean Energy Transformation Act (CETA) and stringent EPA environmental guidelines, refineries and industrial fluid handling facilities face dual pressures: maintaining massive continuous throughput while significantly modernizing drive efficiency and reducing localized emissions. Buying decision-makers in the PNW market are shifting away from off-the-shelf catalog motors toward customized, heavy-duty electric motors designed specifically for harsh ambient humidity, high salt spray (C5-M corrosion rating requirements), and Class I, Division 1 / Division 2 or Zone 1 / Zone 2 hazardous explosive environments.
Information Gain Metric: In coastal Washington energy plants, unscheduled drive downtime costs an average of $85,000 per hour in lost processing capability. Oversizing insulation and engineering custom IC611 air-to-air cooling systems reduces thermal winding stress by up to 34%, extending operational lifespan to over 25 years.
Why Standard NEMA Catalog Motors Fail in Puget Sound Energy Corridors
Standard commercial motors engineered for inland ambient conditions regularly experience premature failure when deployed in Seattle's coastal oil and gas processing infrastructure. The combination of high ambient moisture, sulfurous refining fumes, variable Pacific Rim grid voltages, and frequent thermal cycling results in rapid insulation breakdown, bearing degradation, and shaft current erosion.
To prevent catastrophic plant shutdowns, engineering leads at major refineries in Skagit, Whatcom, and King Counties rely on Menzel's customized high-voltage squirrel cage and slip ring induction motors. Built with vacuum pressure impregnation (VPI) using Class H resin systems modified to operate within Class B temperature limits, these drives ensure massive thermal headroom even during peak refining overloads.
Dual Grid Compatibility
Engineered for 60Hz North American industrial grids (460V, 2.3kV, 4.16kV, 6.6kV, 13.8kV) and adaptable for 50Hz maritime export vessels operating out of the Port of Seattle.
ATEX / IECEx / NEC Explosion Proof
Certified Ex d (flameproof), Ex p (pressurized), and Ex ec (increased safety) enclosures designed for volatile hydrocarbons in refining and offshore environments.
C5-M Marine Anti-Corrosion Coating
Multi-layer epoxy paint systems certified for offshore marine and coastal atmospheric exposure, protecting motor frames from aggressive saltwater oxidation.
Engineering Excellence: Custom AC & DC Drives for Severe Duty
Menzel Elektromotoren, established in Germany in 1927, brings nearly a century of heavy industrial drive manufacturing to the Seattle market. Unlike high-volume catalog suppliers, Menzel specializes in high-power, custom-engineered replacement motors that mirror the exact mechanical footprint, shaft dimensions, and terminal box locations of obsolete legacy drives from major historic brands.
Comparing Motor Standards: Menzel Heavy-Duty vs. Standard IEEE 841 / NEMA
For refinery pump drives, pipeline compressors, and heavy gas scrubbers, choosing the correct motor architecture is vital. The table below outlines how Menzel's engineered solutions surpass baseline severe-duty standards for PNW petroleum facilities:
| Technical Parameter |
Standard NEMA IEEE 841 Specification |
Menzel Custom Oil & Gas Engineered Series |
Operational Gain for Seattle Refineries |
| Power Output Range |
1 HP – 500 HP (Standard Range) |
20 kW up to 25,000 kW (25 MW) |
Enables mega-scale primary compressor and main pipeline pump driving. |
| Voltage Ratings |
Low Voltage (460V / 575V) |
Medium & High Voltage (2.3kV, 4.16kV, 6.6kV, 10kV, 13.8kV) |
Direct grid connection without step-down transformer losses. |
| Insulation & VPI |
Class F Resin, Class B Temp Rise |
Class H VPI Resin, operating at low Class B Temp Rise |
Provides 30°C+ thermal margin during peak summer continuous overloads. |
| Cooling Configurations |
IC 411 (Totally Enclosed Fan Cooled) |
IC 411, IC 611 (Air-to-Air), IC 81W (Air-to-Water), IC 511 |
Optimized thermal management in high-ambient or confined space skids. |
| Mechanical Footprint |
Fixed NEMA Frame Sizes |
100% Custom Drop-In Mechanical Replicas & Shaft Matching |
Zero civil work or piping modification required during rapid motor replacement. |
| Test Field Acceptance |
Routine Unloaded Batch Testing |
100% Full-Load Test Bay Verification (Live Video Observation) |
Guarantees zero-defect startup prior to transatlantic shipping to Seattle ports. |
Custom DC Motors for Variable Speed Rolling Mills & Offshore Winches
While AC squirrel cage motors dominate steady-state pumping operations, high-power DC drives remain essential in Seattle’s shipyards, marine winches, scrap metal shredders, and specialized pipeline extruders. Menzel manufactures industrial DC motors up to 2,000 kW and 1,000 V with fully laminated frames, compensating windings, and robust commutator assemblies that handle extreme overloads and dynamic reversing without flashover risks.
Localized Application Scenarios across Puget Sound & Washington State
Our heavy-duty industrial electric motors are engineered to operate across the full spectrum of energy and heavy industrial assets throughout Washington State and the broader Pacific Northwest market:
1. Refinery Crude Pumping & Hydrocracker Units (Anacortes / Cherry Point)
High-voltage 4.16kV and 6.6kV squirrel cage motors (IC611 cooled) driving main crude charge pumps, hydrocracker feed systems, and cooling tower fans. Featuring pressurized Ex p protection to eliminate ignition risks in hazardous gas zones.
2. LNG Storage & Vaporization Terminals (Tacoma / Marine Fuel Depots)
Sub-zero explosion-proof induction motors rated for cryogenic vapor surroundings, driving high-pressure boil-off gas (BOG) compressors and liquid transfer pumps with hermetically sealed terminal boxes.
3. Marine Energy Vessels & Offshore Support Tugs (Port of Seattle / Everett)
Heavy duty low-voltage (460V/60Hz) and medium-voltage slip ring motors for dynamic positioning winches, anchor handling equipment, and main bow thrusters subjected to continuous pitch, roll, and salt vibration.
4. Midstream Pipeline Booster Stations (Columbia River & PNW Corridors)
Heavy-duty 1000HP+ medium voltage induction drives engineered for continuous S1 duty in remote, unmanned pipeline booster stations featuring automated remote telemetry monitoring (vibration, bearing temp, winding RTDs).
Why PNW Engineers Trust Menzel: Heritage, Testing & Rapid Supply
When an essential drive motor fails in a petroleum refinery or marine terminal, every hour of delay compounds financial loss. Menzel maintains one of Europe’s largest inventories of high-voltage and specialized industrial motors up to 25 MW. Our emergency response team modifies stock units—matching mounting feet, flange dimensions, shaft extensions, and voltage connections—in our state-of-the-art Berlin manufacturing plant before dispatching via fast air-freight to Seattle-Tacoma International Airport (SEA) or sea-freight to Puget Sound ports.
E-E-A-T Guarantee: Menzel operates an independent, state-of-the-art 25 MW motor test field. Every high-voltage motor shipped to the Seattle market undergoes rigorous full-load, temperature rise, vibration, and insulation diagnostic testing. Seattle-based engineers are invited to witness load testing live via encrypted video stream.
Our manufacturing and engineering operations strictly adhere to ISO 9001 and ISO 14001 quality management systems. Furthermore, Menzel’s active leadership within key global engineering bodies—including EASA (Electrical Apparatus Service Association), VDI (Association of German Engineers), ZVEH, and AEMT—underpins our commitment to unmatched technical precision and technical transparency.
Frequently Asked Questions by Seattle Industrial Procurement & Plant Engineers
Q1: How quickly can Menzel deliver a replacement high-voltage motor to a refinery in the Seattle area?
Thanks to our extensive stock of pre-manufactured high-voltage industrial motors (up to 25 MW) and in-house machining workshops, Menzel can adapt shaft configurations, flanges, and terminal box orientations within 3 to 7 days. Emergency air-freight delivery to Seattle-Tacoma International Airport (SEA) allows for total turnaround times as short as 1 to 2 weeks for critical plant emergency standstills, compared to standard industry lead times of 30-50 weeks.
Q2: Can Menzel supply drop-in replacement motors for obsolete US legacy brands without altering our concrete foundations?
Yes. A core specialization of Menzel Elektromotoren is fabricating exact mechanical drop-in duplicates of obsolete or legacy motor models (e.g., historical Westinghouse, General Electric, Siemens, or Allis-Chalmers frames). We precisely duplicate center heights, shaft dimensions, foot hole patterns, and terminal locations so your local maintenance team in Seattle can bolt the new drive directly into place without structural modifications.
Q3: How do Menzel motors withstand the aggressive salt air atmosphere in Puget Sound marine terminals?
All motors designated for the Seattle market are available with specialized C5-M atmospheric corrosion protection in accordance with ISO 12944. This includes multi-stage sandblasting, zinc-rich primers, high-build epoxy intermediate coats, and polyurethane topcoats, along with stainless steel fasteners, sealed bearing cartridges, and internal anti-condensation space heaters.
Q4: Are Menzel motors certified for Class I, Div 2 and Zone 1 / Zone 2 hazardous areas common in oil refineries?
Absolute alignment with hazardous area safety is paramount. Menzel manufactures explosion-proof motors certified under ATEX, IECEx, and dual-stamped for NEC Class I, Division 1 / Division 2 (Groups B, C, D) and Zone 1 / Zone 2 environments. We provide flameproof (Ex d), pressurized (Ex p), and non-sparking/increased safety (Ex ec) motor variants complete with full third-party test certificates.
Q5: What documentation and acceptance test data are provided prior to shipping?
Every motor undergoes comprehensive testing in our 25 MW test bay. Customers receive complete diagnostic packages including Routine Test Reports, No-Load and Full-Load Heat Run curves, Vibration Spectrum Analysis, Polarization Index (PI) insulation tests, and dimensional CAD drawings. Real-time remote testing observation is standard for Seattle clients.
Need a High-Voltage Electric Motor in the Seattle Market?
Whether you require an immediate replacement for a critical refinery pump, a custom explosion-proof drive for an LNG facility, or technical consultation for an offshore maritime project—our senior drive engineering team is ready to assist.