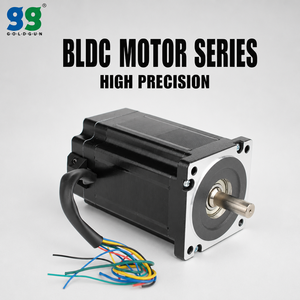
Industrial Automation DC Motors for Electric 48V 750W 110mm BLDC Brushless Motor Permanent Magnet Motor Brushless 2KW
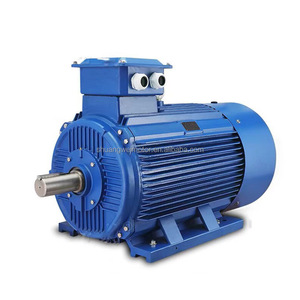
30kw 45kw 55kw 75kw 160kw 200kw 2800rpm 380v AC Three Phase Induction Totally Enclosed High Efficiency 50/60HZ Electric Motor
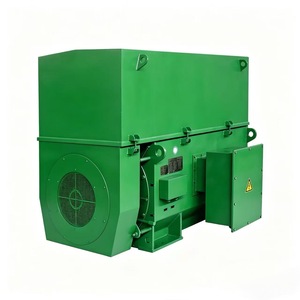
Three-Phase Medium Voltage Induction Motor 3kv 6kv 10kv High Voltage AC for Power Plant Boiler Fan IE3 IP55 Protection 50/60Hz
220V/240V Commercial Kitchen Hood Exhaust Fan Motor Replacement Kit 60Hz Single-Phase Frequency Kitchen Vent Electric Motors
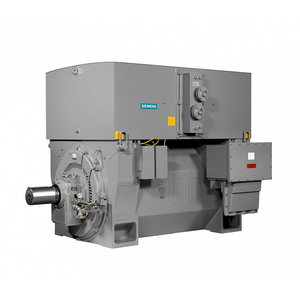
3300v 5500v 6600v Medium Voltage Motor Siemens High Voltage 1000hp Electric Motor Ac Induction Motor
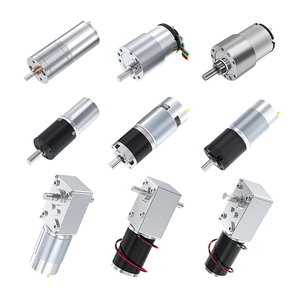
Customize DC Gear Motor 3V 6V 18V 36V 48V Electric Micro RC Planetary Brushless Brushed Gearbox Motors With Gear Box
YKK YRKK 3300v 4160V 5500V 6000V Ac Induction Motor 150KW-9000kw Medium Voltage Motor
Ac Induction Electric Motor 3phase Supplier 18.5kw 22kw 30kw 45kw 55kw 75kw 160kw 200kw 2800rpm 220v 380v
Custom OEM Mechanical & Electrical Retrofitting
100% mechanical drop-in replacements engineered to duplicate obsolete British Standard motor footprints (Mather & Platt, GEC, Brook Crompton) without shaft or foundation modifications.
Full-Load Test Field up to 25 MW / 13.8 kV
Every custom mining motor undergoes rigorous load testing, vibration analysis, and thermal rise inspection. UK clients are invited to witness testing live or via state-of-the-art digital streams.
ATEX, UKCA & Underground Explosion Protection
Full compliance with UK Health & Safety Executive (HSE) mining codes, offering Ex d, Ex p, Ex ec, and M1/M2 underground flameproof enclosures for hazardous dust and gassy mine shafts.
Engineering High-Capacity Mining Electric Motors for the United Kingdom Market
The UK heavy extraction, quarrying, and mineral processing sectors are experiencing a major technological transition. With major mining projects in Cornwall (Lithium hydrometallurgical extraction), North Yorkshire (Potash and Polyhalite shaft mining), and extensive stone, limestone, and aggregate quarrying across the Mendip Hills and Scotland, industrial drive infrastructure must deliver continuous high-torque performance under relentless operational stress.
As a global OEM factory and premier exporter serving the United Kingdom, our manufacturing architecture bridges the gap between legacy British motor installations and next-generation power electronics. When standard catalog motors fail to meet severe-duty mechanical or electrical demands, custom OEM engineering provides the required power density, thermal headroom, and longevity.
Addressing Extreme Operating Conditions in UK Mining & Extraction
Heavy industrial operations within the UK present unique environmental and grid challenges that standard off-the-shelf industrial drives cannot withstand:
- Aggressive Ambient Corrosion & Moisture: Underground shaft dewatering systems and coastal extraction plants require specialized VPI (Vacuum Pressure Impregnation) winding protection using Class H synthetic resins, combined with IP66 or IP67 ingress seals to prevent moisture penetration.
- Severe Mechanical Shock & Radial Stress: Jaw crushers, cone crushers, and SAG mills subject motor shafts and bearing assemblies to massive transient shock loads. Our custom OEM designs incorporate high-tensile forged alloy shafts, spheroidal graphite iron end-shields, and heavy-duty roller bearings with ceramic insulation to eliminate VFD-induced fluting.
- Gassy Explosive Atmospheres (Methane & Combustible Dust): Mining operations must strictly adhere to the UK Health & Safety Executive (HSE) Mines Regulations 2014 and UKCA/ATEX directives. Flameproof Ex d enclosures and pressurized Ex p topologies ensure zero ignition risks in underground shafts.
Custom Replica Drops-In: Eliminating Downtime in UK Industrial Plants
A primary challenge facing UK plant managers and maintenance leads is replacing legacy electric motors originally manufactured by GEC, Mather & Platt, English Electric, or older Brook Crompton lines. Modern standard IEC motors feature smaller frame sizes and different shaft center heights, requiring expensive civil and mechanical modifications to existing baseplates.
Our custom OEM factory specializes in manufacturing drop-in replica motors. By engineering custom steel base adapters, matching historic shaft extensions, terminal box positioning, and flange dimensions, we allow UK engineers to unbolt damaged legacy drives and drop in a brand-new high-voltage modern unit within hours—maximizing uptime and saving thousands of pounds in structural retrofitting.
Energy Efficiency, UKCA Compliance & Net-Zero 2050 Alignment
Under the UK Energy Information regulations and decarbonization targets, high-capacity motors operating continuous duty cycles must meet IE3 and IE4 efficiency thresholds. Optimizing copper volume in the stator slots, utilizing low-loss electrical steel laminations, and applying CFD-designed internal cooling fans significantly reduce internal losses.
Over a typical 20-year operational life of a 5 MW mine ventilation fan, electricity costs account for over 90% of total lifecycle expenses. Upgrading to high-efficiency custom OEM motors dramatically lowers Total Cost of Ownership (TCO) while helping UK extraction operators achieve their carbon reduction metrics.
Q: Can you build a drop-in replacement for obsolete UK motor frame sizes?
Yes. We specialize in custom OEM shaft extensions, custom foot mounting positions, and terminal box alignments to replicate legacy British Standard motor frames (e.g., GEC, Mather & Platt) without requiring foundation modification.
Q: Are your hazardous area mining motors UKCA and ATEX certified?
Absolutly. Our Ex d (flameproof), Ex p (pressurized), and Ex ec motors are certified according to UKCA and ATEX standards for Zone 1, Zone 2, Zone 21, Zone 22, and underground M1/M2 gassy mining environments.
Q: How do your high-voltage motors handle variable speed drive (VFD) operation?
All VFD-duty motors feature VPI insulation reinforced against high dV/dt voltage spikes, insulated non-drive-end bearings (or hybrid ceramic bearings), and Faraday shielding to eliminate shaft current bearing damage.
Q: What cooling method is best suited for dusty UK quarry mill crushers?
IC611 (Air-to-Air heat exchanger) is ideal for heavy dust environments as it isolates the inner winding circuit from airborne dust. Where water cooling is available, IC81W offers a highly compact frame with low noise.
Q: What is the typical dispatch timeframe for UK emergency motor delivery?
We maintain one of Europe's largest stock holdings of large industrial motors up to 25 MW. In emergency plant standstill scenarios, stock units can be modified in-house and dispatched to UK ports or job sites within 24 to 48 hours.
Q: Do you provide full factory acceptance testing (FAT) before shipment?
Yes. Every motor is tested at our on-site load test field (up to 25 MW / 13.8 kV). We issue complete type-test reports according to IEC 60034-1, and UK engineers can join the test live via secure digital links.