Direct Factory Supply for Russian Heavy Machinery, Mining, Metallurgy, and High-Voltage Plant Infrastructure
In the modern global industrial drive landscape, the demand for China wholesale heavy duty gear motors has transitioned from standard mass-produced power units to highly specialized, custom-engineered torque transmission systems. Russian heavy industry—spanning Northern Siberian mining, Ural metallurgical complexes, Volga oil refineries, and Far Eastern port logistics—presents some of the world's most severe operational environments. Drive equipment must operate reliably under sustained continuous duty (S1), heavy shock loads (up to 250% overload), extreme ambient temperature swings ranging from -60°C to +40°C, and highly corrosive or explosive atmospheres.
As a premier Chinese OEM/ODM gear motor manufacturer with nearly a century of cumulative engineering legacy and strong technical partnerships with Russian industrial procurement networks, our manufacturing architecture combines European precision gear design with China's robust, cost-effective industrial manufacturing ecosystem. This whitepaper analyzes the essential mechanical, electrical, thermal, and regulatory parameters involved in selecting, procuring, and deploying high-capacity gear motors and high-voltage induction drives across the Russian Federation.
Engineering Specifications for Shock Resistance, High Output Torque, and Extended Service Life
Our heavy-duty gearboxes utilize high-grade carburizing alloy steels such as 20CrMnTi and 17CrNiMo6. Pinions and gear wheels undergo precise vacuum carburizing, quenching, and CNC gear grinding to achieve gear surface hardness of HRC 58-62 while maintaining a ductile core. This architecture offers exceptional resistance to pitting fatigue, bending stress, and extreme shock loads generated by industrial crushers and ball mills.
Gearbox housings are cast from high-density gray iron HT250 or nodular cast iron QT450-10, engineered via finite element analysis (FEA) to maximize structural rigidity. The rigid box structure absorbs torsional vibration, maintains internal gear alignment under heavy radial forces, and minimizes acoustic emissions during high-power transmission.
Equipped with auxiliary cooling circuits including IC411 (Self-Ventilated), IC611 (Air-to-Air heat exchanger), and IC81W (Air-to-Water cooling), our heavy-duty drive systems effectively dissipate thermal energy generated during continuous heavy loads, preventing lubricant breakdown and maintaining optimum stator winding insulation integrity.
| Gear Type Series | Input Power Range | Output Torque (Nm) | Ratio Range | Primary Industrial Application |
|---|---|---|---|---|
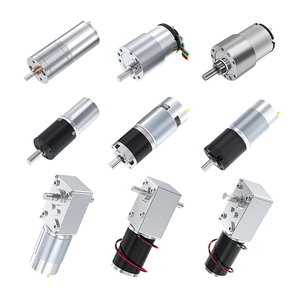
| R Series Helical Gear Motors | 0.12 kW – 160 kW | Up to 18,000 Nm | 1.3 – 27,000 | Pumps, Agitators, Light Conveyors, HVAC Systems |
| K Series Helical-Bevel Gear Motors | 0.12 kW – 200 kW | Up to 50,000 Nm | 5.36 – 33,000 | Steel Rolling Mills, Mining Conveyors, Heavy Hoists |
| S/F Series Parallel Shaft / Helical Worm | 0.18 kW – 90 kW | Up to 12,000 Nm | 6.8 – 22,800 | Material Handling, Food Processing, Mixers |
| P Series Industrial Planetary Gearboxes | 5.5 kW – 2,000 kW | Up to 2,600,000 Nm | 25 – 4,000 | Heavy Cement Kilns, Bucket Wheel Excavators, Winches |
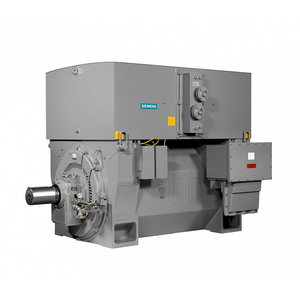
| YKK/YRKK MV High Voltage Motors | 150 kW – 9,000 kW | Custom High Torque | Direct / VFD Driven | Power Plant Boiler Fans, Mine Ventilation, Compressors |
Proven Performance in Siberian Permafrost, Metallurgical Mills, and Arctic Offshore Facilities
In open-pit coal mines and underground nickel extraction sites throughout Kuzbass and Norilsk, conveyor drive heads and ore crushers operate under relentless abrasion and sub-zero temperatures.
Metallurgical complexes in Magnitogorsk, Chelyabinsk, and Yekaterinburg require gear motors capable of managing continuous shock impact, radiant heat from white-hot steel billets, and high ambient humidity.
From the Yamal Peninsula LNG extraction facilities to Volga region refineries, electrical drives must meet stringently monitored explosion protection standards and variable speed drive (VFD) compatibility.
Seamless Procurement, Import Substitution, EAC Certification, and Logistics Optimization
Over the past several years, Russian industrial enterprises have accelerated the transition from Western European OEM equipment (such as SEW-Eurodrive, Siemens, and Flender) to premium Chinese motor and gearbox manufacturers. Chinese factories have responded by developing exact drop-in dimensional replacements for standard European frame sizes, shaft center heights, bolt-hole patterns, and flange dimensions.
This technical alignment ensures Russian plant operators can replace failed gearboxes or retrofitted drives without requiring costly structural modifications or civil foundation re-engineering.
Exporting industrial electrical drives into the Russian Federation, Belarus, and Kazakhstan requires strict adherence to Technical Regulations of the Customs Union (TR CU). Our factory-certified production lines hold complete compliance documents:
German Engineering Principles Combined with China's Advanced Scale Manufacturing
Every custom high-voltage motor and industrial gearbox undergoes comprehensive acceptance testing prior to dispatch. Our state-of-the-art test field supports full-load, temperature rise, vibration analysis (ISO 10816), partial discharge testing, and acoustic noise measurements. Overseas clients can participate via live video stream or on-site inspections.
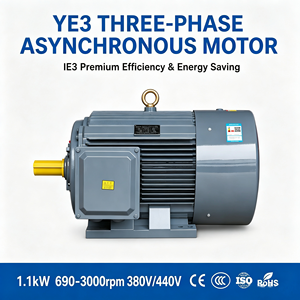
We maintain one of Asia's largest inventories of semi-finished castings, shaft steel, stator core laminations, and standard winding wire. Whether you need standard IEC 75kW induction motors or a non-standard 6000V slip ring motor with customized shaft extensions, our rapid manufacturing schedule cuts delivery lead times by up to 50%.
Our dedicated export division manages direct rail transport via Manzhouli / Zabaykalsk, direct sea routes to Vladivostok, and overland trucking to Moscow, Saint Petersburg, Yekaterinburg, and Novosibirsk. Complete export documentation, custom tariff clearance codes (HS Codes 8501 / 8483), and certified timber packaging compliant with ISPM 15 are fully standard.
Technical, Regulatory, and Procurement Clarifications for Engineers and Supply Chain Managers
Yes. We engineer direct dimensional drop-in replacements for major European and Asian drive lines. Shaft diameters, keyways, center heights, foot mounting holes, and output flange dimensions match standard international standards (IEC/DIN). We provide 2D/3D CAD drawings prior to manufacturing to verify 100% mechanical interchangeability.
For extreme cold climate operation (HL and UHL climate categories according to GOST 15150-69), we utilize synthetic low-temperature lubricants, low-temp Fluorosilicone/Viton oil seals, space heaters within the motor housing to prevent condensation, and impact-resistant ductile iron (QT450) or low-temperature carbon steel casings to avoid cold brittleness.
Absolutely. All gear motors and high-voltage electrical machinery exported to Russia are supplied with full EAC TR CU certificates (TR CU 004/2011 for low voltage, TR CU 020/2011 for EMC, TR CU 010/2011 for machinery safety, and TR CU 012/2011 for explosion-proof equipment). We provide all documentation in both English and Russian.
We supply motors wound for standard Russian industrial power grids, including low-voltage 380V/660V (50Hz), 220V/380V (50Hz), as well as medium and high-voltage grids of 3kV, 3.3kV, 6kV, 6.6kV, 10kV, and up to 13.8kV. Motors designed for Variable Frequency Drives (VFD) are equipped with insulated non-drive end bearings and Class H insulation.
Standard induction motors and stock gearbox frames ship within 7 to 15 days. Custom engineered heavy-duty gearboxes or high-voltage motors (above 1 MW) require 30 to 45 days. Shipments are dispatched via direct rail freight (14-20 days to Moscow/Ural regions) or sea-rail multimodal via Vladivostok.
All industrial drives come with a standard 18-month factory warranty or 12 months of active operational warranty. We supply spare parts packages (pinion shafts, gear sets, bearings, terminal boxes) and maintain technical support channels to assist on-site Russian engineering teams with commissioning and maintenance.
For inverter-fed duty (VFD), high-frequency shaft currents can cause fluting in motor bearings. We mitigate this by integrating ceramic insulated bearings at the non-drive end (NDE), installing copper grounding brushes at the drive end (DE), and applying shielded VPI insulation with inverter-grade magnet wire.
Our heavy-duty motors are fitted with PT100 platinum resistance temperature detectors (RTDs) embedded directly into stator windings (2 per phase) and bearing housings. Additionally, PTC thermistors and bimetallic thermal switches can be installed according to customer control system specifications.
Looking for custom gear motor engineering, rapid OEM replacement units, or bulk factory wholesale supply for projects in Russia or worldwide? Our senior drive application engineers are ready to assist you with torque calculations, drawings, and competitive direct quotes.