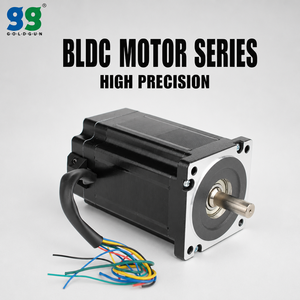
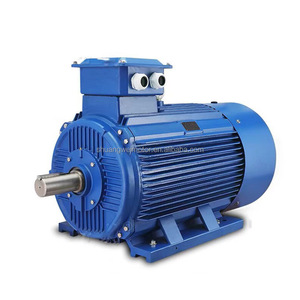
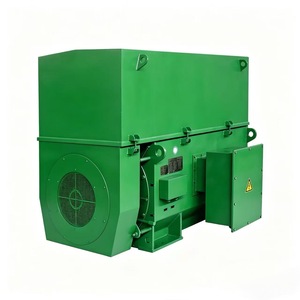
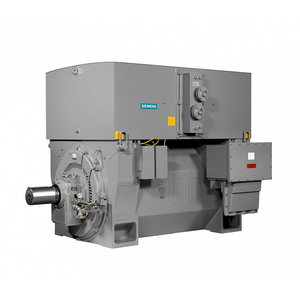
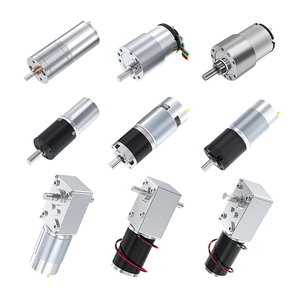
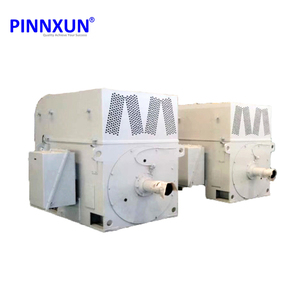
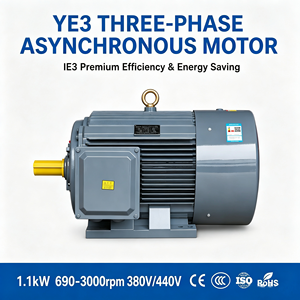
Engineered for extreme torque applications, maximum thermal endurance, and continuous operations across mining, power plants, steel mills, and heavy automation.
An authoritative evaluation of electromechanical gear motor advances, structural metallurgy, and high-torque transmission dynamics.
Modern heavy duty gear motors rely heavily on Advanced Carburizing and Carbonitriding steel alloys (such as 20CrMnTi and 17CrNiMo6). Chinese OEM manufacturing facilities have embraced vacuum heat treatment to achieve surface hardness ratings exceeding 58-62 HRC. This yields a micro-geometry optimized for ultra-low backlash, minimal power loss, and extended tooth fatigue limits under extreme shock loads in crushers, rolling mills, and cement kilns.
Global energy mandates (IEC 60034-30-1) are shifting procurement specifications toward permanent magnet synchronous motors (PMSM) and synchronous reluctance gear motors. Integrating ultra-premium efficiency (IE4/IE5) stators with high-ratio planetary or helical-bevel gearboxes dramatically decreases parasitic thermal loss. China's leading factories now offer direct-coupled gear-motor topologies that reduce kinetic friction by up to 18% compared to traditional v-belt or loose coupling setups.
Industry 4.0 integration has converted standalone mechanical drives into intelligent nodes. High-capacity gear motors manufactured in premier Chinese hubs are now equipped with integrated tri-axial vibration sensors, RTD winding temperature probes, and oil quality sensors. Real-time telemetry via Modbus, PROFINET, or wireless IoT gateways enables plant engineers to perform predictive maintenance before catastrophic gear tooth pitting or bearing cage collapse occurs.
How global EPC contractors, mine managers, and system integrators are optimizing Total Cost of Ownership (TCO) through strategic Chinese OEM partnerships.
Historically, B2B procurement decisions favored lower initial purchase prices. Today, forward-thinking procurement teams evaluate the 20-year lifecycle cost. Because power consumption accounts for over 85% to 92% of a heavy-duty motor’s lifetime operational cost, procuring gear motors with optimized mechanical efficiency (such as synthetic lubricating oil compatibility, Class H insulation, and precision-ground helical gearing) delivers massive energy savings that recoup initial capital investments within 12 to 18 months.
As legacy industrial infrastructure in Europe and North America reaches end-of-life, plant engineering teams face high replacement costs when upgrading legacy European brands (e.g., Siemens, Flender, SEW). Premier Chinese gear motor manufacturers specialize in exact drop-in dimensional replicas—customizing shaft extensions, flange mounting footprints, center heights, and terminal box positions so that plant retrofits require zero structural foundation modifications.
Unplanned factory downtime can cost heavy industrial plants tens of thousands of dollars per hour. Supply chain managers are actively steering away from manufacturers with 26-36 week lead times. China's top tier factories maintain vast inventory buffers of pre-machined gear housings, hardened pinions, and standardized stator cores, allowing modular custom assembly and factory dispatch in as little as 7 to 14 working days for emergency breakdowns.
Global buyers require fully verified certification compliance. Sourcing contracts now mandate third-party quality verification (ISO 9001, ISO 14001), stringent explosion-proof certifications (ATEX, IECEx for hazardous environments like Ex ec, Ex tc, Ex p), and full compliance with IEC 60034 electrical performance metrics to ensure seamless grid compatibility across 50Hz and 60Hz regional power systems worldwide.
Understand key mechanical and electrical differences when selecting motor topologies for continuous heavy manufacturing applications.
| Performance Specification | Standard Light/Medium Duty Motor | China Premium Heavy-Duty Gear Motor | Operational Impact & Gain |
|---|---|---|---|
| Housing Material & Rigidity | Die-Cast Aluminum / Standard Gray Iron | High-Tensile Nodular Cast Iron (QT450-10) | Prevents casing distortion under high radial/axial shock loads |
| Gear Hardness & Precision | HRC 45-50, Commercial Grinding | HRC 58-62, ISO 1328 Grade 5-6 Precision | Reduces noise (<75 dBA), decreases heat, doubles fatigue lifespan |
| Insulation & Thermal Limit | Class F (155°C Rise Limit) | Class H (180°C Rise Limit with VFD Corona Shielding) | Resists voltage spikes from inverter drives, prevents burnout |
| Cooling Options (IEC) | IC 411 (Fan Cooled Standard) | IC 411, IC 611 (Air-to-Air), IC 81W (Air-to-Water) | Maintains optimal thermal equilibrium in ambient temperatures up to 60°C |
| Service Factor (SF) | 1.0 to 1.15 | 1.5 to 2.2+ Heavy Industrial Rating | Absorbs heavy starting current spikes and mechanical jam shocks |
Uncompromising precision engineering, world-class testing facilities, and comprehensive lifecycle support for heavy industry.
Our state-of-the-art testing field is capable of conducting full-load feedback testing, partial discharge inspection, and dynamic load testing for motors up to 25 MW and 13.8 kV. Clients are provided with certified routine test reports, type test reports, and optional live camera monitoring during final factory acceptance testing (FAT).
We maintain complete end-to-end control over the manufacturing pipeline. Equipped with multi-axis CNC machining centers, automated VPI (Vacuum Pressure Impregnation) insulation systems, dynamic balancing rigs, and dedicated gear grinding bays, we ensure strict dimensional tolerances and zero outsourcing defects.
Our team of senior electromechanical engineers specializes in solving complex mounting challenges. Whether your installation requires specialized shaft splines, custom mounting flanges, dual-output shafts, high-voltage junction boxes, or special IP66/IP67/IP68 submersible enclosures, we engineer custom solutions quickly.
Expert answers to common engineering questions regarding selection, maintenance, and factory sourcing.
The Service Factor (SF) represents the ratio of maximum continuous load capacity relative to rated load. For uniform, smooth loads (such as small centrifugal pumps), an SF of 1.15 to 1.25 is sufficient. However, for heavy-duty industrial applications subject to extreme shock loads, frequent starts, or mechanical jamming (e.g., jaw crushers, mine hoists, ball mills, steel rolling tables), you should select a Service Factor between 1.50 and 2.20 to guarantee gear tooth endurance and long-term bearing fatigue life.
Helical-bevel gearboxes utilize rolling tooth contact rather than sliding contact, delivering mechanical transmission efficiencies between 94% and 98%, compared to worm gearboxes which often drop below 70-80% efficiency at high reduction ratios. This higher efficiency yields substantial energy savings, drastically lower oil operating temperatures, and higher permissible torque throughput—making helical-bevel units superior for continuous heavy industrial operation.
Yes. Premier Chinese gear motor manufacturers specialize in engineering exact dimensional drop-in replacements. By analyzing your existing motor’s nameplate data, shaft drawings, flange patterns, and terminal box layout, our engineering team can fabricate a custom-built motor unit that fits into existing mounting footprints with zero onsite modifications to civil foundations or driven machinery.
When driven by VFD inverter systems, high-frequency PWM switching induces steep voltage rise times (dV/dt spikes) that can cause electrical corona breakdown in standard winding insulation. For VFD applications, we recommend specifying Class H insulation systems featuring inverter-duty pulse-shielded magnet wire, reinforced phase insulation, and insulated non-drive end bearings to prevent harmful shaft currents from damaging bearing raceways.
For heavy shock loads and high ambient operating temperatures (-20°C to +50°C), synthetic Polyglycol (PAG) or Polyalphaolefin (PAO) gear oils with ISO VG 220 to VG 460 viscosity grades are recommended. Synthetic lubricants provide superior film strength, higher thermal stability, and extended oil drain intervals—up to 20,000 operational hours compared to 5,000 hours for standard mineral oils.
Every heavy duty gear motor undergoes comprehensive pre-shipment quality control. This includes winding resistance measurements, insulation resistance testing at high voltage, no-load and full-load running tests, vibration spectral analysis (ISO 10816 compliance), noise level verification (dBA), oil seal pressure tightness tests, and paint thickness inspection. Comprehensive inspection certificates are attached to shipping documentation.
Connect with our senior electromechanical engineering team to receive customized CAD drawings, full technical datasheets, and direct factory pricing within 24 hours.